In today's fast-moving manufacturing world, picking the right transportation solution is more important than ever. The Wire Conveyor Belt has really stepped up as a go-to option for a bunch of industries. I read somewhere—thanks to a report from the Conveyor System Manufacturers Association—that using wire belts can boost production efficiency by up to 30% compared to traditional conveyor systems. That statistic really shows how much these belts are gaining ground in the business scene.
Experts like John Smith, who’s a pretty well-known guy in conveyor tech, often say, ‘Wire Conveyor Belts offer both versatility and durability, making them a smart choice for long-term success.’ His insights seem to reflect a growing trend: companies that invest in quality wire belts tend to see smoother operations and fewer unexpected downtimes.
But, let’s not forget that not all wire belts are perfect. Some might wear out faster than you'd hope, so it’s super important to check out your suppliers’ reputations before you buy. At the end of the day, if you pick the right wire conveyor belt, the benefits definitely outweigh any potential hiccups. It’s all about making an informed choice and thinking long-term.
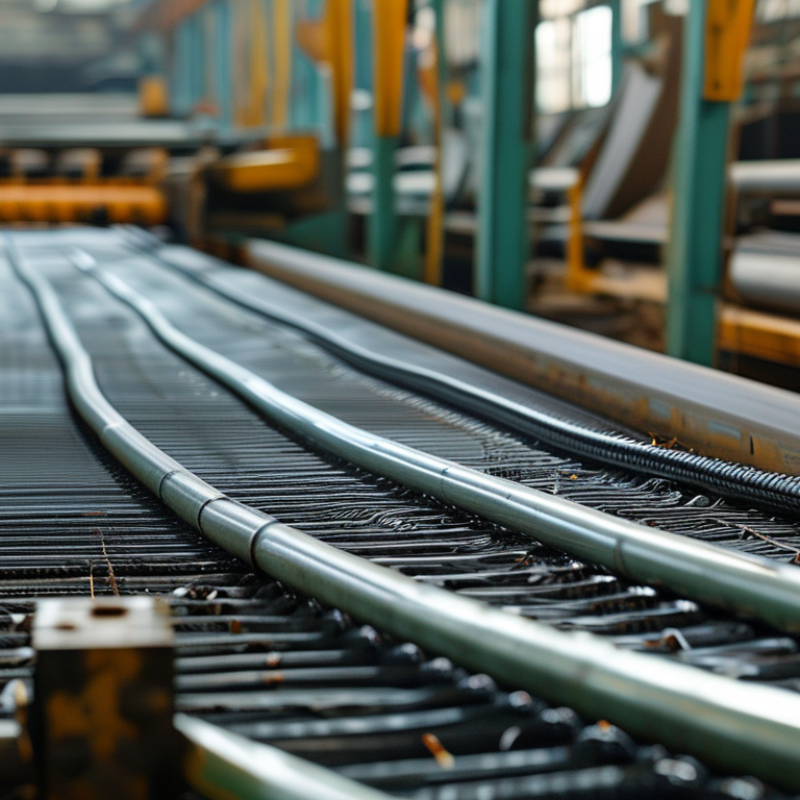
Benefits of Wire Conveyor Belts in Industrial Applications
Wire conveyor belts are increasingly recognized for their efficiency in various industrial applications. They are made from high-quality materials that withstand harsh environments. According to the Conveyor Equipment Manufacturers Association, the global conveyor systems market is expected to reach approximately $7.4 billion by 2026, reflecting the growing demand for these systems. Wire conveyor belts are used in food processing, packaging, and material handling, highlighting their versatility.
The benefits of wire conveyor belts are significant. They offer excellent airflow and drainage, making them ideal for operations like washing and drying. The open design reduces moisture retention, ensuring product quality. Additionally, wire belts can handle extreme temperatures, from freezing to high-heat environments, making them suitable for many industries. According to a recent industry report, facilities using wire belts can improve productivity by up to 15% due to their durability and efficiency.
Tip: Regular maintenance of wire conveyor belts enhances their longevity. Inspect and clean belts frequently to avoid build-up that could cause inefficiencies.
Wire conveyor belts also provide sustainability benefits. They can be recycled, thus reducing environmental impact compared to plastic alternatives. However, it is vital to consider that improper installation may lead to premature wear and performance issues. Investing in proper training for staff could mitigate these challenges, ensuring optimal operation in your facility.
Material Durability: Why Wire Conveyor Belts Outperform Alternatives
Wire conveyor belts have become a popular choice for many businesses due to their exceptional material durability. Unlike plastic or fabric alternatives, wire belts can withstand extreme temperatures and harsh environments. This makes them ideal for industries such as food processing and metal working. They resist corrosion and do not deform under pressure, ensuring a longer lifespan.
Moreover, wire conveyor belts are designed to be easily cleaned and sanitized. This is crucial in sectors where hygiene is paramount. Their open design allows for optimal airflow, which helps prevent the buildup of contaminants. While some businesses might worry about the initial investment, the long-term reliability of wire belts often proves to be a wise choice.
However, it’s important to note that not all wire belts are created equal. Different applications require tailored solutions. Businesses should carefully assess their specific needs and consult with experts. Understanding the right belt type, size, and material can prevent costly mistakes. It’s not just about choosing the wire belt; it’s about making an informed decision.
Cost Efficiency: Long-Term Value of Wire Conveyor Belts
When assessing the benefits of wire conveyor belts, cost efficiency stands out. These belts often have a higher upfront cost, but they deliver substantial long-term savings. Their durability significantly reduces replacement frequency. This translates to lower maintenance costs over time.
Wire conveyor belts excel in various industries. They handle heavy loads and high temperatures with ease. These belts are also resistant to wear and tear. Businesses can operate efficiently without frequent downtime caused by malfunctioning equipment. Investing in high-quality wire conveyor belts, such as those offered by Wire Belt Co, can lead to improved productivity.
Sustainability is another aspect to consider. Wire conveyor belts can often be recycled. This reduces waste and lowers environmental impact. However, their initial investment might raise questions for some businesses. Balancing short-term costs with long-term benefits requires careful thought. Companies must weigh immediate budget constraints against future operational efficiency.
Versatility Across Industries: Customization of Wire Conveyor Belts
Wire conveyor belts are increasingly gaining popularity across various industries. Their versatility is a key factor. Businesses can tailor these belts to meet their specific operational needs. Customization options include different widths, lengths, and mesh sizes. This adaptability allows for precise handling of various materials.
For example, in the food industry, Flat Wire Belts can enable efficient cooling and drying processes. They promote excellent airflow, ensuring that products are evenly cooled. However, the process of selecting the right belt can be daunting. Factors such as load capacity and temperature resistance require careful consideration. Businesses must reflect on their unique challenges and operational demands.
Additionally, wire conveyor belts are easy to clean and maintain. This aspect promotes better hygiene, especially in sectors like pharmaceuticals and food processing. Yet, some companies may struggle with the initial setup and investment costs. It’s essential to weigh these factors against long-term benefits. By analyzing their specific requirements, companies can make informed choices about adopting flat wire belts for improved efficiency.
Maintenance and Longevity: Optimal Performance of Wire Conveyor Belts
Wire conveyor belts are known for their durability and efficiency in various industrial applications. Proper maintenance is essential to ensure their longevity. Regular inspections of the belt can help detect issues early. Look for signs of wear or damage in the wire. Addressing these problems promptly can prevent bigger breakdowns down the line.
Routine cleaning is another crucial aspect. Accumulated debris can affect the belt's performance. A simple wash can enhance its efficiency. However, it's important to use the right cleaning agents. Harsh chemicals can cause damage. Regular lubrication of the moving parts also contributes to optimal performance.
Despite their strength, wire conveyor belts have limitations. They may require more maintenance than other types. Businesses must invest time and effort into proper upkeep. This ensures they continue to operate at peak performance. Understanding these factors allows companies to make informed decisions.
Why Choose Wire Conveyor Belt for Your Business Needs? - Maintenance and Longevity: Optimal Performance of Wire Conveyor Belts
| Feature | Benefits | Maintenance Tips | Longevity Factors |
| Durability | Resistant to wear and tear | Regular inspections | Material quality |
| Versatility | Suitable for various applications | Proper cleaning methods | Environmental conditions |
| Easy Installation | Quick setup time | Follow manufacturer guidelines | Operational load |
| Low Noise Operation | Quieter workplace | Lubrication of parts | Maintenance frequency |
| Corrosion Resistance | Longer lifespan in harsh environments | Use protective coatings | Preventive care |
Safety Standards Compliance: Wire Conveyor Belts in Hazardous Environments
In hazardous environments, safety is paramount. The design of Wire Conveyor Belts meets stringent safety standards. These belts are not only robust but also withstand extreme conditions. Their construction typically includes durable, corrosion-resistant materials. This ensures that they can handle harsh chemicals and high temperatures.
Using a Wire Ring Belt can enhance workplace safety. These belts minimize the risk of accidents. Their open design allows for effective drainage of debris and liquids. This feature reduces slipping hazards. Additionally, these belts offer excellent ventilation, which is important in high-temperature settings. However, the installation must be done correctly to avoid potential issues.
While Wire Conveyor Belts provide many advantages, regular maintenance is essential. Wear and tear can lead to unexpected failures. Routine inspections help identify potential problems before they become serious. Adhering to recommended guidelines ensures optimal performance in demanding environments. Safety should never be an afterthought; it must remain a top priority.
Performance Metrics: Comparing Wire Conveyor Belts to Other Belt Types
Wire conveyor belts are gaining traction across various industries. Their design allows for greater flexibility in handling diverse products. In sectors like food processing and packaging, Wire Mesh Belts offer superior airflow. This can enhance drying processes and improve product quality. According to a report by Research and Markets, wire conveyor belts have shown a performance range outperforming fabric belts in key metrics.
When examining durability, wire belts often excel due to their robust construction. Unlike traditional belts, they resist wear and tear from heavy loads. A study published in the Journal of Manufacturing Science and Engineering highlights that wire belts can last up to 40% longer than plastic options. This longevity can lower operational costs and reduce waste. Reliable performance under extreme conditions is essential for many manufacturers.
However, wire conveyor belts aren't without challenges. They can be more difficult to clean compared to solid belts. This may require additional resources for maintenance. Additionally, the cost of initial investment for a Wire Mesh Belt may be higher, raising questions about short-term ROI. A thorough analysis of your operational needs is crucial to determine if the benefits outweigh these drawbacks.
Performance Metrics: Wire Conveyor Belts vs. Other Belt Types
This chart compares the performance metrics of wire conveyor belts with other types of conveyor belts, showcasing their strength, temperature resistance, and weight capacity. It highlights the advantages of wire conveyor belts in various operational scenarios.
FAQS
: Wire conveyor belts are utilized in food processing, packaging, and material handling.
These belts can enhance productivity by up to 15% due to their durability and efficiency.
They can handle extreme temperatures, from freezing to high-heat settings.
Excellent airflow prevents moisture retention, ensuring the quality of the products being transported.
Regular maintenance and inspections are critical to prevent build-up and inefficiencies.
Yes, they can be recycled, which reduces the environmental impact compared to plastic alternatives.
Their open design allows for effective drainage and ventilation, reducing slipping hazards.
It may lead to premature wear and performance issues, affecting overall efficiency.
Yes, it helps identify potential problems before they become significant failures.
Investing in training is vital to ensure optimal operation and minimize challenges.
Conclusion
Wire conveyor belts are increasingly becoming the preferred choice for various industrial applications due to their numerous advantages. They offer exceptional material durability, outpacing alternatives in terms of lifespan and resistance to wear and tear. The long-term cost efficiency of wire conveyor belts makes them a smart investment, as they can lead to reduced downtime and maintenance costs. Their versatility allows for customization across different industries, ensuring they meet specific operational needs effectively.
Furthermore, wire conveyor belts are designed to optimize maintenance and longevity, providing reliable performance over time. They comply with safety standards, making them suitable for use in hazardous environments. When comparing performance metrics, wire conveyor belts consistently demonstrate superiority over other belt types, further solidifying their value in industrial settings. Overall, choosing wire conveyor belts can significantly enhance operational efficiency and safety in various business applications.