In the world of logistics, Conveyor Belt Transportis pretty much a game-changer when it comes to streamlining operations. I remember John Smith, a logistics pro at BeltTech Solutions, once saying, "A well-designed Conveyor Belt System can really change how we handle materials." That quote pretty much sums up how powerful these systems can be when it comes to boosting productivity.
Now, conveyor belt systems aren’t just about moving stuff from point A to B; they're a real mix of innovation and efficiency. They handle all kinds of materials—heavy goods, tiny packages—you name it. Plus, they help cut down on human errors and make workplaces safer. That said, they’re not perfect. Maintenance can get pretty tricky, and if the design isn’t just right, you might end up with bottlenecks that slow everything down.
The industry’s always changing, too. New tech is making these systems smarter with real-time monitoring and automation, which sounds awesome. But, of course, this means we’ve got to rethink some of the old ways of doing things. As we dive into how Conveyor Belt Transport works, we’ll check out how they operate, the benefits they bring, and some of the pitfalls to watch out for. Basically, it’s all about getting a clear picture of one of the most vital parts of modern logistics.
What is a Conveyor Belt? An Overview of Its Definition and Purpose
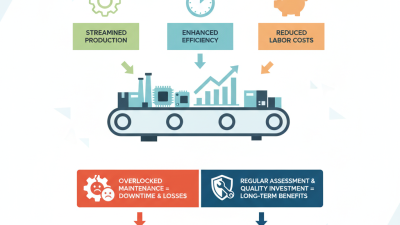
A conveyor belt is a crucial tool in Material Handling. It's designed to transport items efficiently across varying distances. Conveyor belts are widely used in industries like manufacturing, logistics, and mining. Their purpose is to reduce labor costs and increase productivity. According to a report by the Conveyor Equipment Manufacturers Association, market trends show a steady growth, with an expected increase of around 4.5% annually through 2026.
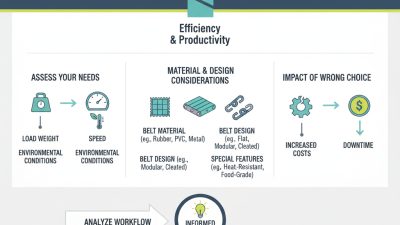
The basic components of a conveyor belt include the belt itself, pulleys, and rollers. Belts can be made of various materials to suit different loads and environments. For instance, rubber belts are common in heavy-duty applications, while fabric belts work for lighter loads. However, the ideal choice often requires careful consideration. Improper selection can lead to safety hazards and increased maintenance costs.
**Tips:** Consider the load type and weight when choosing a conveyor belt. Regular inspection is essential to maintain efficiency. Ensure that the belt is suited for the specific application to avoid unnecessary downtime. Small errors in selection can result in significant operational issues later.
History of Conveyor Belt Transport: From Inception to Modern Applications
The conveyor belt transport system has evolved significantly since its inception. Initially, the first conveyor belts were created in the late 18th century, primarily for agriculture. They were simple, made of wood and leather. As industries developed, so did the technology behind these belts. Today, conveyor systems are utilized in sectors ranging from mining to food processing.
In the 20th century, continuous improvements shaped modern applications. By the 1950s, the use of rubber belts began to dominate, enhancing durability and efficiency. Reports show that the global conveyor systems market is expected to reach $10 billion by 2025. The need for reliable transportation solutions drives this growth. Specific applications, such as the Fly Ash Transport Belt 600°C, showcase how tailored designs can handle extreme temperatures in power generation.
Despite technological advances, challenges exist. Many existing systems face maintenance issues. Understanding how friction, wear, and material degradation affect performance is crucial. Addressing these problems can significantly impact operational efficiency. Continuous innovations are essential to adapt to evolving industrial needs while ensuring safety and reliability in different environments.
How Conveyor Belts Work: Basic Principles and Mechanisms Explained
Conveyor belts are essential for modern industries. They transport materials efficiently across various distances. Understanding how they work is fundamental for optimizing production processes.
Conveyor belts operate on basic principles of motion and friction. A continuous loop of flexible material moves around pulleys. When the power is applied, the belt moves. Products placed on the belt are carried from one point to another. The tension in the belt plays a crucial role, as it affects the load capacity and speed. Improper tension can lead to misalignment, causing breakage or jams.
The mechanism involves more than just moving parts. Sensors and control systems can enhance efficiency. These components monitor performance and prevent downtime. Yet, issues like wear and tear are inevitable. Regular maintenance is key, but it is often overlooked. This oversight can lead to costly repairs and disruptions. Understanding these details can help improve reliability and efficiency in operations.
Types of Conveyor Belts: Materials and Designs for Various Needs
Conveyor belts play a crucial role in modern transport systems. Different types of conveyor belts serve various industrial needs. They are designed from a range of materials, each offering unique benefits. For instance, rubber belts provide excellent grip and durability, making them suitable for heavy loads. Fabric belts, on the other hand, are lighter and more flexible, ideal for less demanding applications.
When choosing a belt, it's important to consider the environment. Plastic belts resist corrosion, while Metal Belts excel in high-temperature settings. These materials can influence efficiency and safety. For example, if aTransport Conveyor is used in wet conditions, a non-slip surface might be necessary. A poor choice can lead to costly delays and accidents.
Not all designs fit every application. Some belts have grooves or ribs to enhance item stability. Others are flat, promoting easy loading and unloading. Although these designs seem straightforward, the complexities of engineering a reliable system often go unnoticed. Examining various factors ensures optimal performance for specific tasks within any facility.
Common Applications of Conveyor Belts in Different Industries
Conveyor belts play a crucial role in various industries. They transport materials efficiently across different production stages. In manufacturing, conveyor belts enhance productivity. A report by the International Journal of Industrial Engineering notes that efficient transport systems can boost output by up to 30%. This efficiency is essential where time and cost are key factors.
The mining industry heavily relies on conveyor belts. They move ore from extraction sites to processing facilities. A study found that using conveyor systems reduces transportation costs by nearly 20%. However, maintenance can be a challenge. Wear and tear on belts create downtime, and it’s vital for companies to regularly inspect their systems.
In warehouse operations, conveyor belts streamline the sorting and shipping process. A report from Logistics Management highlights that automated systems improve order fulfillment speed by 25%. Yet, improper use can lead to accidents. Training employees on safe practices is essential. The balance between efficiency and safety remains a topic of reflection in the industry.
Maintenance and Safety Considerations for Conveyor Belt Systems
Maintaining conveyor belt systems is crucial for efficiency and safety. Regular inspections help identify wear and tear before they become serious issues. Operators should check for proper alignment and tension. Misalignment can lead to increased wear and may even cause accidents.
Safety is paramount when working with conveyor systems. Employees must be trained to understand safety protocols. Protective covers should be installed to minimize risks. Additionally, emergency stop buttons should be easily accessible for quick reactions.
Tips: Always conduct a thorough inspection after any maintenance. This ensures everything is functioning correctly. Keep a maintenance log to track repairs and replacements. Regular training sessions for employees can enhance their awareness of potential hazards in the Transport Chain. Creating a culture of safety will lead to more productive operations.
Future Trends in Conveyor Belt Technology and Innovations
The future of conveyor belt technology is rapidly evolving. Innovations focus on enhancing efficiency and sustainability. Environmental concerns drive manufacturers to design belts made from recycled materials. These materials reduce waste and lower production costs.
Smart technology integration is another key trend. Conveyor systems now utilize sensors and IoT devices. These components monitor performance in real-time. Increased data collection allows for predictive maintenance, reducing downtime. Yet, reliance on technology raises questions about cybersecurity threats.
Automation plays a crucial role too. Robotics and AI streamline the sorting and transporting processes. While the benefits are clear, the workforce must adapt to these changes. Continuous training and upskilling become essential. Balancing innovation and human labor is a challenge that requires ongoing reflection.
What is Conveyor Belt Transport and How Does it Work?
| Dimension | Details |
| Conveyor Belt Type | Rubber, PVC, Modular Plastic, Steel |
| Load Capacity | Up to 100 tons per hour |
| Belt Width | From 12 inches to over 60 inches |
| Speed | From 0.5 to 10 m/s |
| Applications | Manufacturing, Mining, Food Processing, Warehousing |
| Maintenance Frequency | Monthly inspections, with more frequent checks during heavy use |
| Innovations | Smart sensors, AI monitoring, Eco-friendly materials |
High-Quality Conveyor Belts from China: Reliable Flat Flex Belt Suppliers for Diverse Industrial Applications
When it comes to material handling in various industrial sectors, high-quality conveyor belts play a pivotal role in ensuring efficiency and safety. Our selection of flat flex belts provides versatile solutions tailored for diverse applications. For instance, the High-Flex Flat Wire Conveyor Belt is crafted from 316L stainless steel, ensuring compliance with FDA safety standards, making it an ideal choice for environments where hygiene is paramount.
In addition to standard options, our range includes specialty belts such as the Anti-Static Flat Flex Belt, which is essential in PCB manufacturing to mitigate static electricity risks. Also noteworthy is our Food-Grade Flat Flex Mesh, which meets stringent EHEDG and USDA certifications for safe food handling, highlighting the importance of regulatory compliance in food processing facilities. According to industry reports, the global conveyor belt market is projected to grow significantly, driven by ongoing advancements in automation across industrial sectors, emphasizing the critical need for reliable and high-performance conveyor solutions.
For those operating in extreme environments, our High-Temperature Flat Flex Belt can withstand continuous operations at temperatures up to 500°C, catering to industries that face severe conditions. Coupled with our Heavy-Duty Flat Flex Belt, designed for robust packaging automation needs, it confirms the adaptability of our product line across various industrial applications. As a trusted supplier in the conveyor belt market, we remain committed to delivering innovative solutions that meet the evolving demands of the industry.
FAQS
: Common materials include rubber, fabric, plastic, and metal. Each has specific benefits based on application needs.
Rubber belts are best for heavy loads due to their grip and durability. They are suitable for demanding environments.
Environmental factors matter. For wet conditions, a non-slip surface is necessary. The wrong choice can lead to issues.
Conveyor belt designs include grooves, ribs, and flat surfaces. Each design serves a unique purpose, affecting stability and loading.
Maintenance prevents wear and tear. Neglecting it can lead to downtime and costly delays in operations.
They streamline sorting and shipping processes. Automated systems can enhance order fulfillment speed significantly.
Conveyor systems reduce transportation costs but require regular inspection due to wear. Maintenance can be a significant challenge.
Efficient conveyor belts can boost production output by up to 30%. This efficiency is vital for competitiveness in the market.
Training should focus on safety practices. Improper use can lead to accidents, reflecting the need for comprehensive training.
Complexities often go unnoticed in designing reliable systems. Ensuring proper function requires attention to various engineering factors.
Conclusion
Conveyor Belt Transport is an essential system used across various industries to facilitate the efficient movement of materials and goods. This method has evolved since its inception, with a rich history detailing its transformation from simple mechanical designs to modern, advanced applications. Conveyor belts operate based on several fundamental principles, employing various materials and designs tailored to specific needs, which enhances their versatility in different operational settings.
In addition to their wide-ranging applications—from manufacturing and logistics to agriculture and mining—effective maintenance and safety practices are crucial for ensuring optimal performance and longevity of conveyor belt systems. Looking ahead, innovations in conveyor belt technology promise to further enhance efficiency, sustainability, and automation in transport processes, marking an exciting future for this vital component of industrial operations.