Leave Your Message
You know, the way manufacturing processes are evolving so quickly these days is pretty incredible. We’re seeing some really cool new uses for Industrial Oven Belts that are actually making a big difference—boosting efficiency and helping keep precision on point in production lines.
According to industry stats, the global conveyor belt market is projected to hit around $6 billionby 2025, mainly because of more automation and the rising demand for advanced manufacturing tech. As a forward-thinking Metal Conveyor belt maker,JIANGSU HUADA Metal Mesh Belt CO., LTD. gets how important it is to have those well-engineered wire mesh belts and chain-driven systems to keep industrial oven processes running smoothly.
With certifications like ISO 9001 and CE, HUADA’s committed to providing top-notch solutions to over 20 countries across five continents—so they’re definitely a major player in pushing manufacturing tech forward.
All in all, adding Industrial Oven Belts into various manufacturing steps not only cranks up productivity but also helps maintain consistent quality—really a big step ahead for the industry.
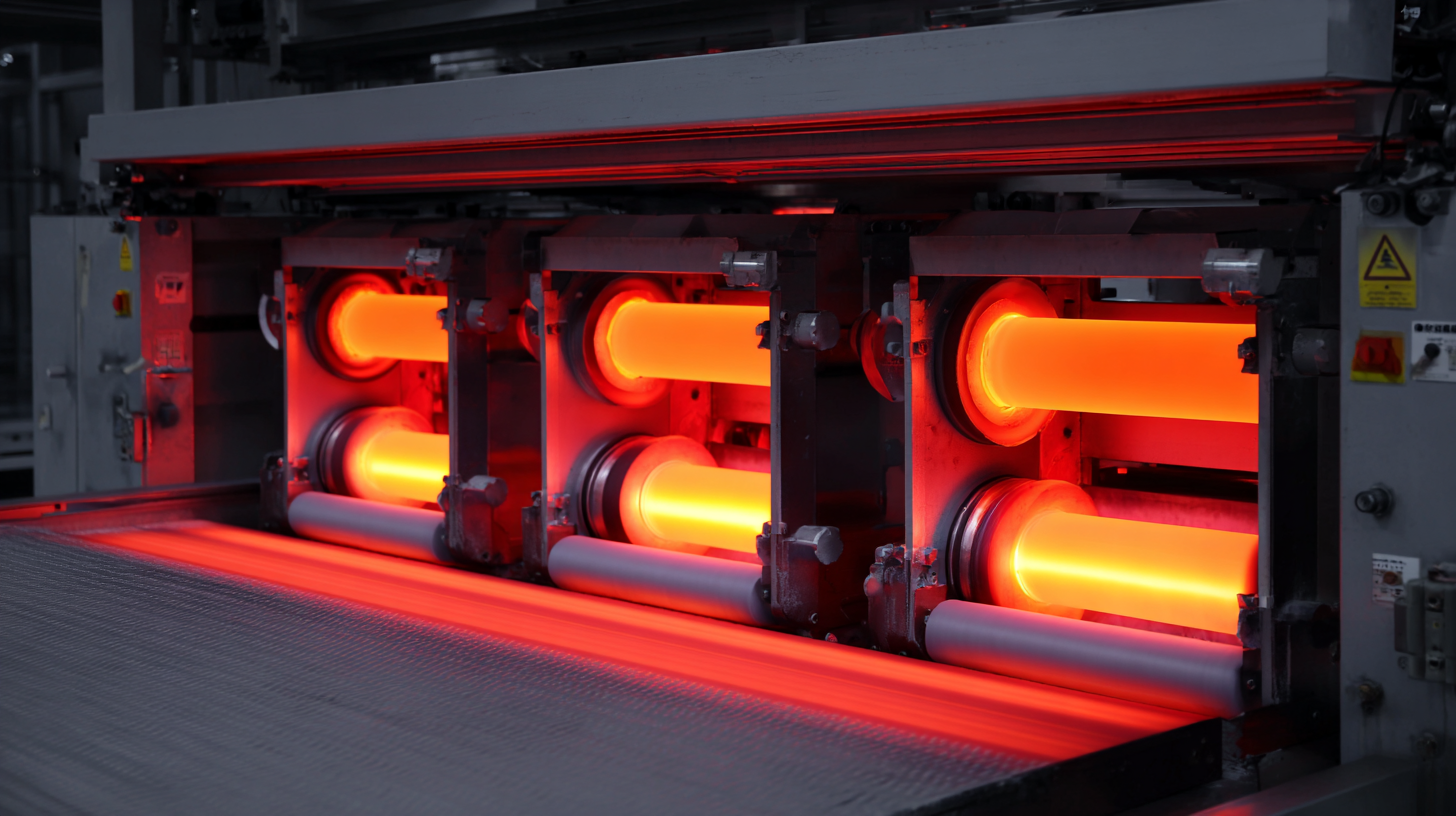
The way industrial oven belts have evolved is a big deal when it comes to making manufacturing run smoother and more efficiently across different industries. Nowadays, there are some pretty cool innovations with these belts, like better heat distribution, longer-lasting materials, and more flexible operation options. Thanks to advances in materials and engineering, manufacturers can really fine-tune their production lines—cutting down on waste and saving energy in the process. Using high-performance metal mesh belts helps products move through the heating stage seamlessly, so you get consistent cooking or drying results and can handle higher volumes without breaking a sweat.
At JIANGSU HUADA METAL MESH BELT CO., LTD., we’re proud to stay at the forefront of these changes. As one of China’s leading metal conveyor belt makers, we supply precisely crafted wire mesh belts and chain-driven systems to over 20 countries around the world. Our ISO 9001 and CE certifications mean our production facilities follow strict quality standards—so you can trust that our solutions are top-notch. By constantly improving our industrial oven belts, we're helping our clients boost their manufacturing efficiency. It’s all about pushing the envelope and doing our part to stay ahead in this competitive global market.
: Innovative industrial oven belts are designed to improve heat distribution, durability, and operational flexibility in manufacturing processes, leading to optimized production, reduced waste, and lower energy consumption.
JIANGSU HUADA METAL MESH BELT CO., LTD. is a leading manufacturer of precision-engineered wire mesh belts and chain-driven systems, supplying solutions that exceed industry standards and help clients improve their manufacturing processes.
Temperature control is crucial for ensuring consistent processing of materials, which directly influences quality and efficiency in manufacturing workflows such as baking, curing, and more.
Advanced temperature control technologies, such as real-time monitoring and feedback systems, allow for dynamic adjustment of heating elements based on thermal load or material flow, enhancing operational precision.
Yes, by minimizing energy waste and reducing downtime and maintenance costs, effective temperature control contributes significantly to energy savings and sustainability in manufacturing practices.
The automotive parts manufacturer achieved a 30% increase in production efficiency and higher quality paint finishes due to improved heat distribution and reduced curing times after implementing a high-performance oven belt.
The bakery utilized a multi-tier oven belt system for consistent temperatures and airflow, resulting in uniform baking of bread products, minimized wastage, and improved customer satisfaction.
Sophisticated temperature management strategies optimize oven belt operations, boost productivity, reduce energy consumption and material waste, and contribute to sustainability in manufacturing.
Industrial oven belts are commonly used in various industries, including food production, textiles, electronics, and automotive manufacturing.
High-performance metal mesh belts allow for seamless product transitions through heating phases, maximizing throughput and ensuring uniform cooking or drying results, which enhances overall manufacturing efficiency.
When it comes to manufacturing, using innovative Industrial Oven Belts has really made a difference in how efficiently things get done. Think of it this way — these belts now come with smarter designs that boost their durability, help spread heat more evenly, and handle heavier loads without breaking a sweat. Because they’re precisely engineered, these belts do a great job keeping the temperature just right during different processes, which means the products turn out consistently good across the board.
There are plenty of stories from different industries showing how these belts are flexible enough to meet specific manufacturing needs. Looking ahead, the whole scene is getting even cooler because smart tech is starting to get integrated into these systems. That’s gonna give manufacturers even more control and precision — pretty exciting, right?
And on that front, JIANGSU HUADA METAL MESH BELT CO., LTD. is right there leading the charge. They’re delivering solutions that are ISO 9001 and CE certified, and they’re used all over the world in various applications. It’s pretty clear that these innovations are reshaping how things are produced — making everything smoother and more reliable.