In today’s fast-changing world of manufacturing, getting those production lines running smoothly has become more important than ever for companies wanting to stay efficient and boost productivity. One of the key players in making this happen is Wire Mesh Conveyor Belt technology. If you look at the market outlook, the global conveyor systems sector is expected to hit around $10 billion by 2027 — mainly fueled by industries pushing for more automation. Now, a big name in this space is JIANGSU HUADA METAL MESH BELT CO., LTD. They’re actually one of China’s first movers when it comes to metal conveyor belts, and they’re making a real impact by providing precision-made wire mesh belts and chain-driven systems. With their ISO 9001 and CE certifications, HUADA supplies reliable solutions to over 20 countries across five continents, helping companies work more smoothly and handle materials effortlessly. So, jumping into wire mesh conveyor belt tech isn’t just a smart move — it’s pretty much essential if you wanna stay competitive in today’s manufacturing game.
Benefits of Wire Mesh Conveyor Belts in Production Environments
Nowadays, in modern production setups, wire mesh Conveyor Belts are really gaining popularity because of all their practical benefits. They’re great at allowing air and liquids to flow through easily, which makes them a top choice for industries that need quick drying—think food processing or textile manufacturing. What’s more, these belts can handle high temperatures and heavy loads without breaking a sweat, so they’re super reliable for different kinds of production tasks. Plus, they’re pretty flexible — it’s easy to tweak and customize them to fit your specific production line needs.
On top of that, their durability and the fact that they’re pretty easy to maintain really help cut down on downtime. Compared to some older conveyor systems, they don’t break down as often or require as much fixing, which means manufacturers can keep things running smoothly and save some cash. Another plus is that because wire mesh belts are modular, replacing or upgrading parts is a breeze. This makes it easier for production lines to stay current with new tech or adapt to changing industry demands. Honestly, if you're looking to make your processes more efficient, jumping on the wire mesh conveyor belt bandwagon is definitely a smart move — it’s a great way to boost productivity and keep things running smoothly overall.
Key Considerations for Choosing the Right Wire Mesh Conveyor Belt
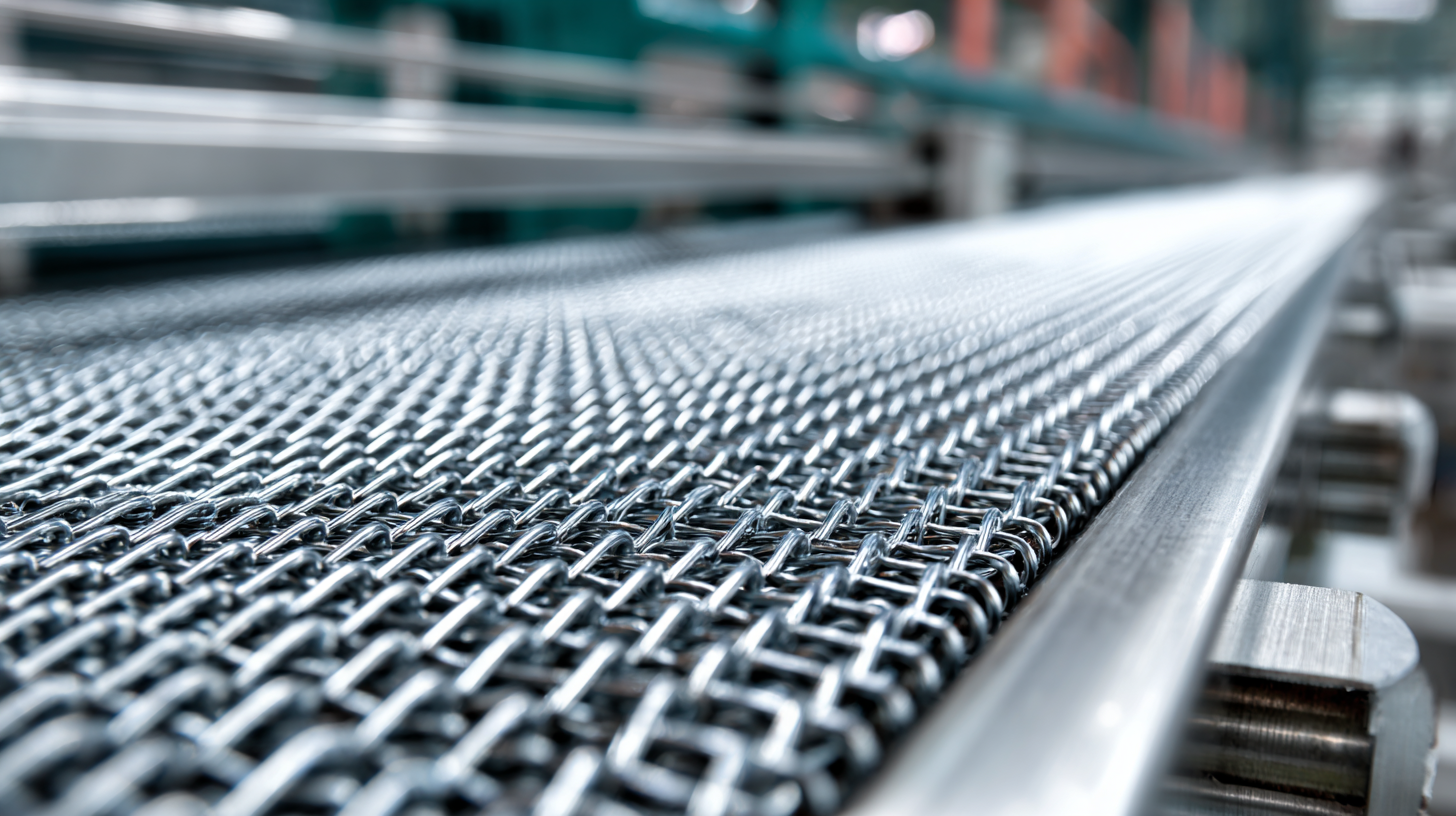
When you're trying to pick the right wire mesh conveyor belt to boost your production line, there are quite a few things you should keep in mind. First off, the material of the belt really matters. Depending on what you're working with, you might need something made of stainless steel, carbon steel, or even some fancy alloys. Each of these has its own perks—like lasting longer, resisting heat, or holding up against corrosion. It’s a good idea to look at your operating conditions too—think about the temperatures involved and if there might be any chemicals in play—to pick a belt that’ll last and perform reliably over time.
Then, there’s the design of the mesh itself. A well-thought-out mesh can really make a difference—improving airflow, cutting down on stuff getting stuck, and making cleaning a breeze. These are pretty important, especially if you're in food processing or pharma where hygiene is a must. Don't forget to consider the size—you want the belt’s width, length, and load capacity to match your production setup. If everything lines up well, you'll keep things running smoothly without unnecessary hiccups.
Bottom line, by paying attention to these details, your business can really make the most out of wire mesh conveyor belts—helping you get more done and keep things running like clockwork.
Techniques for Efficient Installation and Maintenance of Conveyor Systems
In today’s fast-changing manufacturing world, making sure conveyor systems are properly installed and maintained is a big deal if you're serious about keeping production running smoothly. Everyone’s talking about cutting downtime and boosting productivity, right? So, it’s pretty clear that using the right techniques to keep things steady is super important. Studies show that when conveyor systems are well taken care of, you can see throughput jump by up to 25%, and operational costs might drop by around 15% each year. Those numbers really drive home the point: it’s not just about choosing the coolest tech out there, but also about sticking to good maintenance routines and training the staff properly.
At Jiangsu Huada Metal Mesh Belt Co., Ltd., we’re proud to be a leader in this space. We focus on crafting precise wire mesh belts and chain-driven systems that fit a ton of different manufacturing needs. Quality? We don’t cut corners — our ISO 9001 and CE certifications are a testament to that. Regular checks and upgrades, combined with our top-notch wire mesh tech, can seriously keep your operations running at full tilt. Plus, having skilled technicians handle the installation and maintenance makes a huge difference — it’s all about making sure those systems last and that your production hits its full potential, no matter where you are in the world.
Innovative Applications of Wire Mesh Conveyor Belts Across Industries
Wire mesh conveyor belts are really changing the game for lots of different industries, bringing in some pretty cool solutions that boost both efficiency and safety. They’re super versatile too — you can find them in all sorts of designs and materials, which makes them perfect for stuff like food processing, car manufacturing, and pharmaceuticals. One of the best parts? Their open mesh design helps air flow like a charm, so they’re great for drying and cooling. Plus, they can handle heavy loads without feeling bulky, so it’s easy to integrate them into your current production lines without a hassle.
If you’re wondering how to get the most out of these belts, here are a few tips:
1. Pick the right material — whether it needs to stand up to high temps or resist corrosion, choosing the right one can really make your conveyor last longer.
2. Keep up with regular maintenance — a little upkeep goes a long way in keeping everything running smoothly and avoiding costly downtime.
3. Tweak the setup — adjusting things like width, length, or mesh size can really help move your materials along faster and cut down on delays.
All in all, using wire mesh conveyor belts can seriously level up your industry’s productivity and reliability. It’s worth exploring what they can do for you!
Production Line Efficiency by Conveyor Belt Type
Maximizing Productivity: Speed, Durability, and Design Features of Mesh Belts
Wire mesh conveyor belts have really changed the game on production lines. They've boosted efficiency with their speed, toughness, and clever design features. One of the coolest things about these mesh belts is how fast they can run — which means shorter cycle times and higher overall output. That quick pace doesn't just speed things up; it also helps things flow more smoothly between different stages of manufacturing, so you get fewer hold-ups or delays.
Plus, durability is a huge plus with these belts. Made from tough materials, they're built to handle heavy loads and resist wear and tear over time. That means less time and money spent on maintenance or replacements, which is a big win for keeping things running smoothly. Another thing is, the open design of these mesh belts allows for better airflow and drainage — super handy for industries like food processing or metalworking. And if you need something customized, no worries — these belts can be tailored to fit specific production needs, giving you more flexibility on the floor.
How to Optimize Your Production Line with Wire Mesh Conveyor Belt Technology
| Feature | Description | Benefit |
| Speed | High-speed operation with minimal friction. | Increased production output and efficiency. |
| Durability | Constructed from robust materials resistant to wear and tear. | Reduced maintenance costs and longer lifespan of the conveyor system. |
| Design Features | Customizable designs to fit specific applications. | Optimal performance tailored to unique production processes. |
| Versatility | Works with a variety of materials and products. | Flexibility to adapt to changing production needs. |
| Energy Efficiency | Low energy consumption due to efficient design. | Cost savings on energy bills and lower carbon footprint. |
Troubleshooting Common Issues with Wire Mesh Conveyor Belts
When you're working on optimizing production lines with wire mesh conveyor belts, it's really important to be aware of some common issues that can pop up along the way. Honestly, doing regular maintenance and cleaning upfront can save you a lot of headaches later on — stuff that might seem minor, but actually really impacts how smoothly everything runs. Like, if debris builds up, it could cause the belt to go off track or even break down mechanically. Setting up a simple routine to inspect and clean the system helps keep things running without a hitch, so your production doesn’t get stalled.
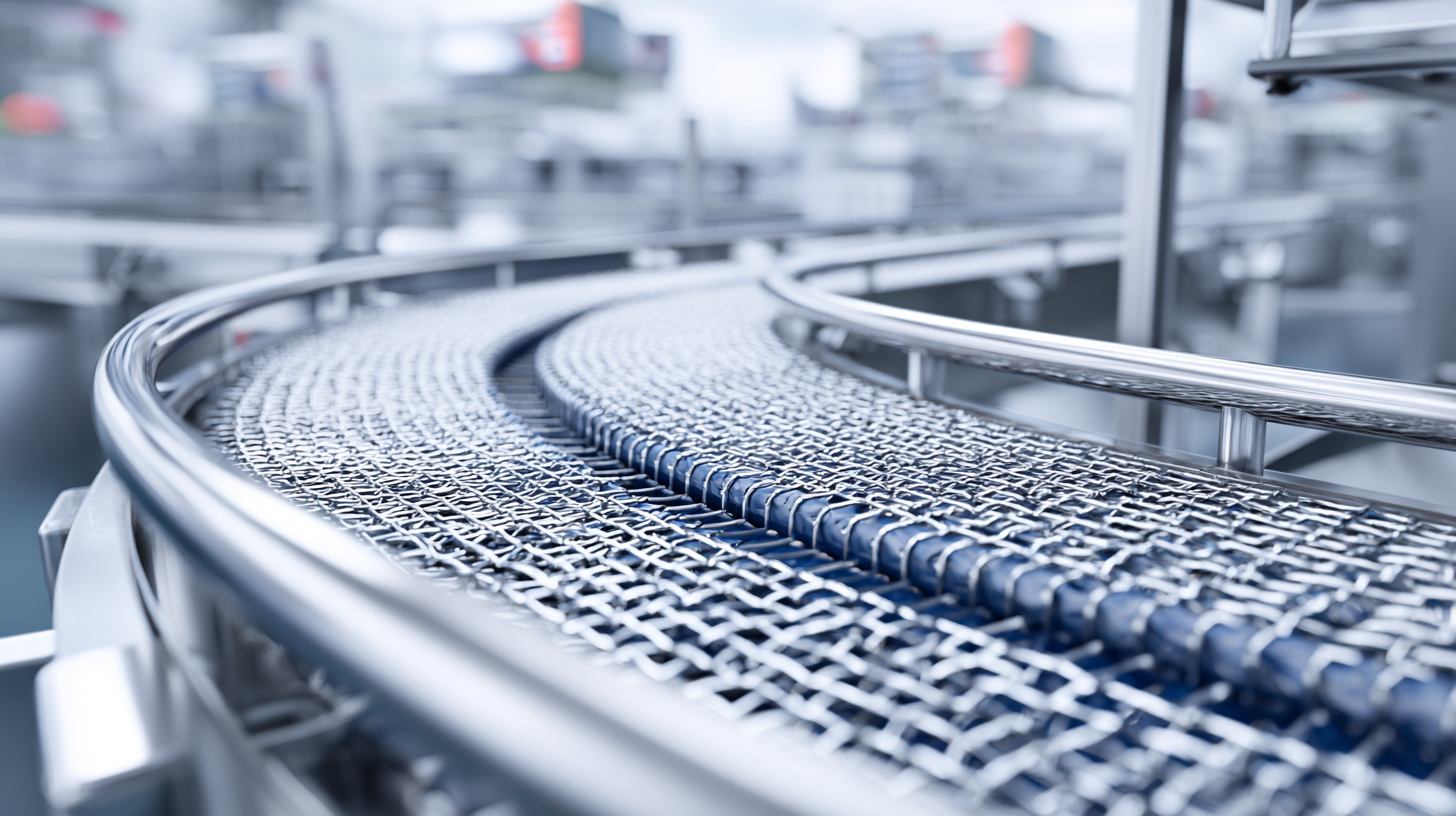
Also, paying attention to things like belt wear or corrosion is super crucial. Keeping an eye on the condition of the wire mesh and replacing parts when needed not only makes the conveyor last longer, but also keeps the workplace safer. By tackling these kinds of issues early, manufacturers can really make sure their production lines run efficiently — making technology work for them, not against them.
Maximizing Efficiency and Versatility with Spiral Conveyor Belts in Modern Industries
In today's competitive industrial landscape, maximizing efficiency and versatility is crucial for success, particularly in food processing and handling sectors. The adoption of spiral conveyor belts has revolutionized these operations, offering enhanced performance across various applications. According to a recent industry report, the market for conveyor systems is expected to grow at a CAGR of 5.2%, highlighting the increasing reliance on innovative technologies, including spiral designs, that cater to diverse processing needs.
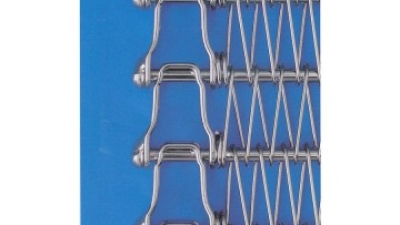
One notable innovation is the Food-Grade Spiral Freezer Belt made from 316L stainless steel, which ensures FDA compliance for food safety—an essential factor in modern food production environments. Additionally, the Low-Temperature Spiral Conveyor Belt, rated to function at -40°C, provides vital solutions for freezing processes in sectors like frozen seafood and vegetable IQF lines. This adaptability not only increases throughput but also reduces energy consumption, aligning with the industry's growing emphasis on sustainable practices. Data indicates that energy-efficient conveyor systems can decrease electricity use by up to 30%, underlining the tangible benefits of upgrading to spiral designs.
Moreover, features such as the Quick-Release Spiral Freezer Belt enhance hygiene practices by facilitating easy cleaning, which is paramount in maintaining the quality standards required in food processing. The emergence of custom-diameter spiral belts allows for optimized space utilization in compact freezer designs, showcasing their versatility across various operational configurations. As industries continue to prioritize efficiency and safety, the role of advanced spiral conveyor belts will likely expand, driving innovation and improving productivity in modern manufacturing.
FAQS
: Wire mesh conveyor belts are versatile conveyor systems made from various designs and materials, ideal for enhancing efficiency and safety in production lines. Their open mesh construction supports air circulation, making them suitable for applications like food processing and automotive manufacturing.
Selecting a belt material that can withstand temperature extremes or corrosive environments based on your specific needs can significantly improve the lifespan of your conveyor system.
Implementing a routine maintenance schedule is essential to ensure optimal performance, reduce downtime, and decrease the risk of malfunctions in conveyor operations.
Tailoring the belt’s design—such as adjusting its width, length, and mesh size—can greatly enhance material flow and reduce bottlenecks in production processes.
Wire mesh conveyor belts can operate at high speeds, which reduces cycle times and increases throughput. They are also constructed from robust materials that resist wear and tear, resulting in lower maintenance costs and infrequent replacements.
These belts are especially effective in food processing, automotive manufacturing, and pharmaceuticals, as well as in operations requiring drying and cooling due to their superior airflow and drainage capabilities.
Customizable design features allow businesses to tailor the belts to meet specific operational needs, enabling flexibility in production line setups and better adaptation to varying processes.
By facilitating high-speed operation, excellent airflow, and customized design, wire mesh conveyor belts help achieve greater productivity and reliability in manufacturing operations.
Conclusion
So, I recently read this article called "How to Optimize Your Production Line with Wire Mesh Conveyor Belt Technology," and honestly, it’s packed with really useful info. It talks about how wire mesh conveyor belts can seriously boost efficiency and productivity in all kinds of production setups. The piece also goes into what you should keep in mind when picking the right belt—things like speed, how durable it is, and clever design features that help keep everything running smoothly. Plus, it shares some handy tips on installing and maintaining these belts, not to mention some pretty cool innovative uses in different industries.
The article also gives a shout-out to Jiangsu Huada Metal Mesh Belt Co., Ltd.—a top player in this field. They really stand out because of their dedication to making precision-engineered solutions, backed by ISO 9001 and CE certifications. With their experience serving over 20 countries around the world, Huada is well-positioned to help businesses fine-tune their production lines with some of the best conveyor tech out there.