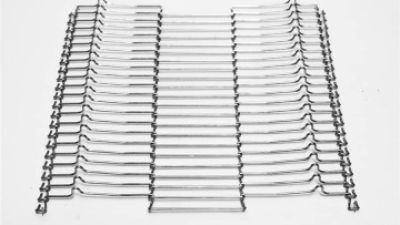
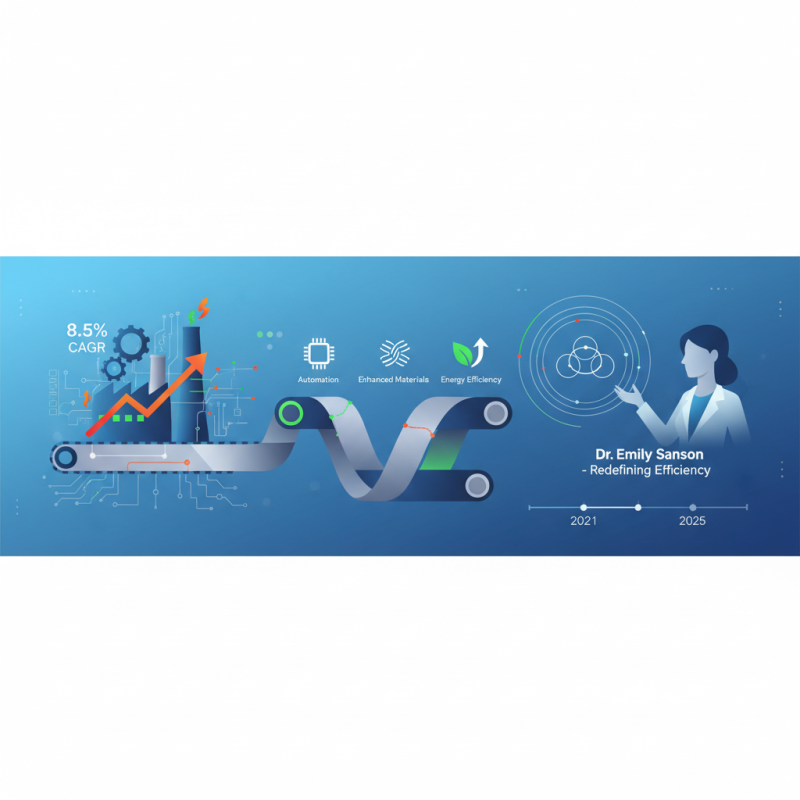
Manufacturing and industrial solutions are changing at a pretty rapid pace these days, and Furnace Belt Companies are definitely leading the way with innovations that are shaping the future of energy efficiency and productivity. I recently came across a report from the Industrial Innovation Institute — quite interesting — which predicted that the furnace belt industry is expected to grow around 8.5% annually from 2021 to 2025. That’s pretty significant growth, and it really highlights just how important it is for folks in the industry to keep up with the latest tech trends and breakthroughs. As companies face mounting pressure to optimize their processes and cut down on environmental impact, the role of innovative furnace belt tech is more critical than ever.
Dr. Emily Sanson, a well-respected expert in thermal processing, put it nicely when she said, “The advancements we see in furnace belt systems today aren’t just small upgrades—they’re actually changing the whole game when it comes to manufacturing efficiency.” Her words really hit the point home and line up well with what recent market studies have been saying, which is that the industry is moving toward more automation, better materials, and smarter energy management systems in furnace belt technology. In this article, I’ll be diving into some of the coolest innovations from Furnace Belt Companies that are expected to really shake things up by 2025 — giving you a peek into what the future of manufacturing might look like.
Cutting-edge Technologies Transforming Furnace Belt Manufacturing
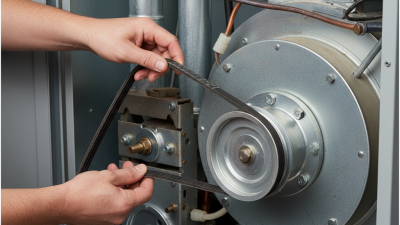
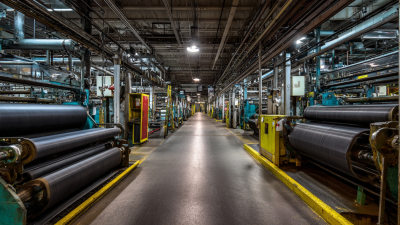
The furnace belt manufacturing industry is witnessing a wave of innovative technologies that are set to transform the way products are created and utilized. One of the most significant advancements is the integration of automation and IoT (Internet of Things) into production processes. This technology not only enhances efficiency but also allows manufacturers to monitor equipment in real time, reducing downtime and ensuring a smoother operation. Additionally, the adoption of advanced materials, such as high-temperature-resistant composites, is improving the durability and performance of furnace belts, enabling them to withstand extreme conditions without compromising functionality.
Tip: When considering the latest innovations in furnace belt manufacturing, always evaluate how these technologies can fit into your existing operations. Investing in automation might require initial adjustments but can lead to significant long-term savings.
Moreover, sustainable practices are becoming increasingly vital in the industry. Manufacturers are focusing on developing eco-friendly furnace belts that minimize energy consumption and reduce waste. For example, using recyclable materials not only caters to the growing demand for sustainable products but also aligns with global efforts to combat environmental issues. Embracing these innovations can not only enhance product offerings but also elevate a company's market position in a competitive landscape.
Tip: Keep an eye out for certifications and eco-labels when sourcing furnace belts; choosing products that meet sustainability criteria can enhance your brand’s reputation while appealing to environmentally conscious customers.
Top Innovations in Furnace Belt Manufacturing (2025)
Recent Innovations in Material Science for Enhanced Furnace Belts
Recent advancements in material science have played a pivotal role in enhancing furnace belt technologies. The development of high-performance composites and specialized alloys enables furnace belts to withstand extreme temperatures and corrosive environments. These innovations focus on improving durability and reducing wear, leading to longer service life and reduced maintenance costs. Research has shown that integrating advanced ceramic materials with conventional metal components significantly increases thermal resistance and structural integrity, making these belts more efficient for industrial applications.
Another noteworthy trend in material science is the introduction of lightweight, high-strength polymers that offer additional flexibility without compromising on performance. These materials not only enhance the operational efficiency of furnace belts by reducing energy consumption but also facilitate easier installation and handling. Moreover, innovations in coating technologies provide enhanced resilience against oxidation and chemical degradation, further extending the lifespan of furnace belts in demanding conditions.
Such developments underscore the importance of ongoing research in material science to support the evolving needs of industrial processes reliant on furnace technology.
Smart Automation: The Future of Furnace Belt Production
The furnace belt industry is undergoing a significant transformation driven by smart automation technologies. With an increasing demand for efficiency and precision, companies are leveraging advancements in artificial intelligence (AI) and the Internet of Things (IoT) to optimize production processes. According to a recent report from the International Data Corporation (IDC), the implementation of smart automation solutions in manufacturing has been projected to boost productivity by up to 30% by 2025. This shift allows for real-time monitoring and adjustment of furnace operations, leading to improved energy efficiency and reduced downtime.
In addition, data analytics plays a crucial role in predictive maintenance, a practice that leverages data to anticipate equipment failures before they occur. A study by McKinsey & Company highlights that predictive maintenance can decrease maintenance costs by up to 25% and reduce unplanned downtime by 50%. By integrating smart automation with data analytics, furnace belt manufacturers can ensure smoother operations and enhance the longevity of their equipment, ultimately driving down operational costs. These innovations not only improve the bottom line but also position companies to respond rapidly to market demands and fluctuations in production cycles.
Sustainability Practices in Furnace Belt Company Innovations
The furnace belt industry is undergoing a transformative shift towards sustainability as companies innovate to reduce their environmental impact. One of the key advancements includes the integration of energy-efficient technologies that not only lower energy consumption during production but also extend the life cycle of furnace belts. By utilizing advanced materials that are both durable and lightweight, manufacturers are minimizing waste and enhancing the efficiency of their products. This focus on sustainability not only addresses ecological concerns but also aligns with the increasing demand for greener options from consumers.
Moreover, many furnace belt companies are exploring circular economy principles, designing products that can be easily recycled or repurposed at the end of their life cycles. This approach not only reduces landfill waste but also creates new opportunities for the reclamation of valuable raw materials. By prioritizing sustainable practices in research and development, these companies are setting new benchmarks in the industry, demonstrating that environmental responsibility and innovation can go hand in hand. As the industry moves towards 2025, the emphasis on sustainability will likely shape not only product offerings but also the operational strategies of furnace belt manufacturers.
Emerging Trends in Energy Efficiency for Furnace Belt Designs
Emerging trends in energy efficiency within furnace belt designs are set to revolutionize the industry by 2025. Recent studies suggest that advancements in material science are pivotal in enhancing the thermal efficiency of furnace belts. According to the International Energy Agency (IEA), energy consumption in industrial heating processes accounts for about 20% of global energy use. By integrating high-performance insulation materials, manufacturers can significantly reduce heat loss, leading to improved overall energy efficiency.
Moreover, the adoption of smart technologies in furnace belt systems is transforming operational landscapes. Data from the American Council for an Energy-Efficient Economy (ACEEE) indicates that implementing IoT-enabled sensors can enhance real-time monitoring and control of temperature variances, thus optimizing energy usage. These systems can adjust the operation based on demand, allowing for significant energy savings of up to 30% during off-peak operations. As these innovations emerge, furnace belt designs are not only becoming more energy-efficient but also paving the way for sustainable manufacturing practices.
Customer-Centric Innovations: Customization in Furnace Belt Solutions
In the rapidly evolving landscape of furnace belt technology, customer-centric innovations are becoming increasingly essential. A recent industry report indicated that customization in furnace belt solutions has surged by 30% over the last few years, driven by the demand for tailored products that meet specific operational needs. This shift towards individualized solutions allows manufacturers to optimize their processes, improving efficiency and product quality. Companies can now offer belts designed with unique materials or configurations that cater to various heating applications, thus enabling them to better serve their clients in diverse industries.
When considering customization, businesses should focus on their unique requirements and operational goals. It's crucial to conduct a thorough analysis of the specific challenges faced in your production processes. By doing this, you can collaborate effectively with manufacturers to develop solutions that are not only reliable but also enhance the overall performance of your systems.
**Tip:** Always keep abreast of advancements in material science as it can significantly influence the performance and durability of your furnace belts. Investing in the latest technologies and materials can provide a competitive edge by reducing maintenance costs and downtimes. Additionally, prioritizing open communication with your suppliers can help in developing bespoke solutions that align not only with current needs but also with future growth plans.
Case Studies of Leading Furnace Belt Companies and Their Innovations
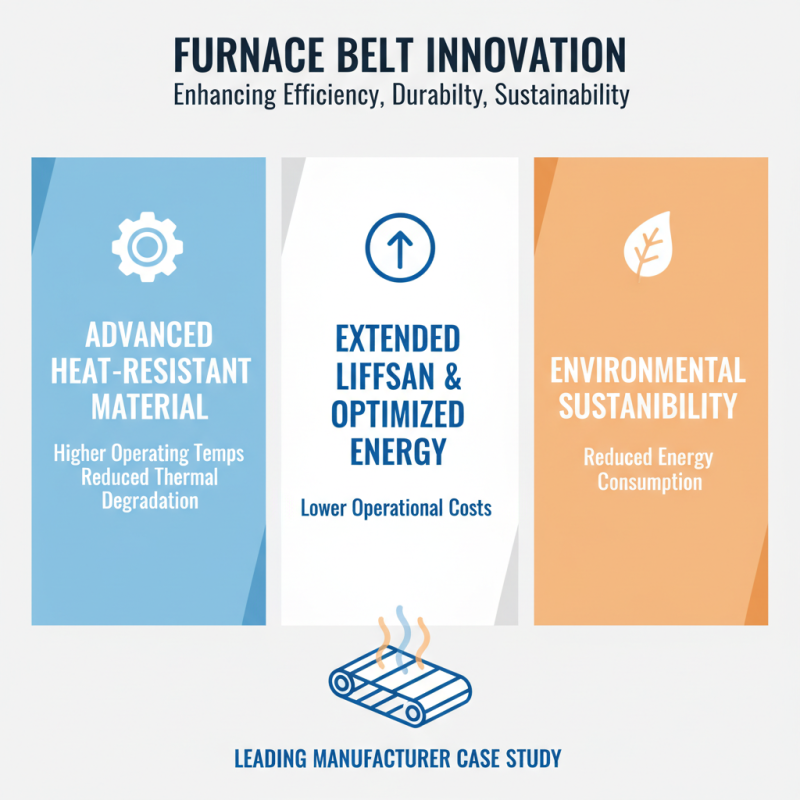
In the competitive landscape of furnace belt manufacturing, several leading companies are pioneering innovations that enhance efficiency, durability, and environmental sustainability. One notable case study focuses on a manufacturer that developed an advanced heat-resistant belt material, allowing for higher operating temperatures and reducing the risk of thermal degradation. This innovation not only extends the lifespan of the furnace belts but also optimizes energy consumption, enabling clients to decrease their operational costs significantly.
Another leading company has introduced a smart monitoring system integrated within its furnace belts. This technology utilizes sensors to track wear and temperature changes in real-time, providing critical data to operators. By leveraging this information, companies can preemptively address maintenance needs, therefore reducing downtime and improving overall productivity. These advancements illustrate how furnace belt companies are not only responding to market demands but also pushing the industry standards forward through their innovative approaches and solutions.
Exploring the Benefits and Features of the Flat Flex Belt for Effective Core Training
The Flat Flex Belt has gained traction in various industries due to its innovative design that enhances efficiency and effectiveness in core applications. In the realm of core training, the versatility of the Flat Flex Belt allows for seamless integration into different manufacturing processes, effectively supporting high-speed operations while ensuring product safety and consistency. With options such as the FDA Compliant High-Flex Flat Wire Conveyor Belt and Food-Grade Flat Flex Mesh, businesses can meet strict regulatory standards, making them ideal for food processing environments.
Furthermore, the use of Low-Profile Flat Flex Belts in small parts assembly illustrates the adaptability of this technology. According to recent industry reports, conveyor belts designed for compact machinery can significantly reduce downtime and improve workflow, thus boosting overall productivity. The incorporation of Anti-Static Flat Flex Belts in PCB manufacturing processes also highlights the importance of tailored solutions for specific industries, as these belts mitigate static buildup that can affect sensitive components.
Moreover, specialized options like Heavy-Duty Flat Flex Belts for packaging automation demonstrate the robustness needed for rigorous applications. Research indicates that using corrosion-resistant materials such as Marine Grade flat flex conveyor can extend the longevity of equipment in challenging environments. The continued evolution and customization of Flat Flex Belts reflect the industry's commitment to improving operational efficiency, while also addressing unique client needs across various sectors.
FAQS
: The shift towards sustainability is driven by the integration of energy-efficient technologies, advancements in material science, and the increasing consumer demand for greener options.
Energy-efficient technologies lower energy consumption during production and extend the life cycle of furnace belts, contributing to reduced environmental impact.
Manufacturers are using advanced materials that are both durable and lightweight to minimize waste and improve the efficiency of their products.
Many companies are exploring circular economy principles, designing products for easy recycling or repurposing at the end of their life cycles to reduce landfill waste.
By focusing on circular economy practices, companies can reclaim valuable raw materials from products at the end of their life cycles, creating new business opportunities.
Innovations include the use of high-performance insulation materials and smart technologies, which can improve thermal efficiency and allow for real-time monitoring of energy usage.
IoT-enabled sensors enhance real-time monitoring and control of temperature variances, optimizing energy usage and allowing for significant energy savings during off-peak operations.
Improving thermal efficiency can lead to reduced energy consumption, which accounts for a significant portion of global energy use, thus contributing to sustainability goals.
Sustainability practices are setting new benchmarks and are likely to shape product offerings and operational strategies, aligning innovation with environmental responsibility.
The adoption of smart technologies can potentially save up to 30% in energy usage during off-peak operations by adjusting system operations based on demand.
Conclusion
The article "Top 2025 Furnace Belt Company Innovations You Need to Know About" highlights the transformative advancements in furnace belt manufacturing, focusing on cutting-edge technologies and recent innovations in material science. As furnace belt companies embrace smart automation, they are streamlining production processes and enhancing efficiency. Sustainability practices are also becoming integral, with an emphasis on eco-friendly materials and energy-efficient designs that cater to modern industrial needs.
Moreover, customer-centric innovations are on the rise, allowing for greater customization in furnace belt solutions tailored to specific operational requirements. The article explores emerging trends in energy efficiency, illustrating how furnace belt companies are adapting to not only meet market demands but also contribute to a sustainable future. Key case studies showcase how leading firms are implementing these innovative practices, setting benchmarks in the industry.