In the world of manufacturing and industrial processes, you really can't overstate how important Industrial Wire Mesh Belts are. These belts are generally reliable and a solid choice when it comes to moving materials around efficiently. Lots of different companies have come up with creative designs to tackle a variety of operational needs, which is pretty cool.
That said, picking the right Industrial Wire Mesh Belt isn’t exactly a walk in the park. There’s a lot to consider because each one has its own specific purpose. For example, you might find belts made especially for food processing, manufacturing, or packaging. But, and here’s the tricky part, not every brand offers the same level of quality or durability. Some belts tend to wear out faster than you'd hope, which can really mess up your production line and cause some headaches. So, it’s a good idea to get a good grip on what’s out there and understand the little differences among the options.
When you're checking out wholesale manufacturers, it’s super important to look into what they actually offer. Brands like Wire Belt Company or Belt Technologies are worth paying attention to. Their products can be pretty different when it comes to specs. To make things easier, you might want to make a checklist—compare materials, load capacity, temperature resistance, stuff like that. But heads up—sometimes that info can get pretty overwhelming or confusing. Finding that sweet spot between quality and cost is often the real challenge, but with a little patience, you’ll get there.
Overview of OEM Wholesale Industrial Wire Mesh Belts
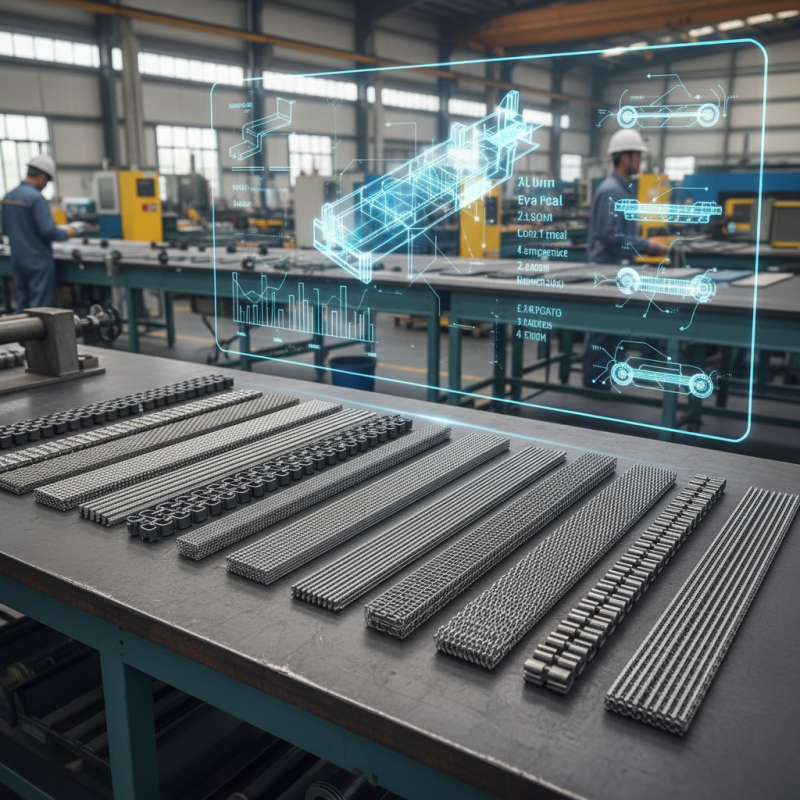
OEM wholesale Industrial Wire Mesh belts play a crucial role in various industries. These belts are essential for processes like sorting, drying, and transporting materials. Their robust construction makes them ideal for handling heavy loads and extreme temperatures.
When choosing an industrial wire mesh belt, consider the wire diameter and mesh size. A tighter mesh may offer better support for smaller items. However, a larger mesh can improve airflow and drainage. Remember, the right choice hinges on your specific application.
**Tip:** Regular maintenance can extend the life of your belt. Clean it frequently to avoid build-up that could lead to wear. Inspect for any damages or wear spots; early detection can save costs.
Selecting the right OEM wholesale products is vital. Each industrial wire mesh belt has unique properties. Ensure it meets your operational requirements. Not all mesh belts are created equal, and misunderstanding their capabilities can lead to inefficiencies.
Top 10 OEM Wholesale Industrial Wire Mesh Belt Products You Should Know
| Product Name | Material | Wire Diameter | Belt Width | Belt Length | Temperature Range | Applications |
| Standard Wire Mesh Belt | Stainless Steel | 2.0 mm | 600 mm | 10 m | -20°C to 600°C | Food Processing |
| Heavy Duty Wire Belt | Carbon Steel | 4.0 mm | 800 mm | 12 m | -10°C to 500°C | Metal Processing |
| Chain Link Mesh Belt | Stainless Steel | 3.0 mm | 1000 mm | 15 m | -20°C to 700°C | Kiln Operations |
| Flat Wire Belt | Stainless Steel | 2.5 mm | 500 mm | 8 m | -20°C to 600°C | Bakery Industry |
| Modular Wire Belt | Plastic | 5.0 mm | 700 mm | 9 m | -10°C to 80°C | Conveyor Systems |
| Timing Wire Belt | Aluminum | 1.5 mm | 600 mm | 11 m | -30°C to 300°C | Automotive Assembly |
| Plastic Spiral Belt | Polypropylene | 3.5 mm | 400 mm | 10 m | -10°C to 90°C | Packaging Industry |
| Welded Wire Mesh Belt | Galvanized Steel | 2.0 mm | 500 mm | 14 m | -20°C to 400°C | Chemical Processing |
| High-Temperature Wire Belt | Inconel | 3.5 mm | 800 mm | 20 m | -200°C to 1000°C | Aerospace Applications |
Key Features of Wire Mesh Belts for Various Industries
Wire mesh belts are essential for various industries, offering unique features that enhance efficiency and safety. Their key qualities include durability, flexibility, and temperature resistance. These belts can handle heavy loads, making them ideal for manufacturing and processing environments. Their resistance to heat allows safe operation in high-temperature applications, such as ovens or dryers.
Different industries benefit from specific types of wire mesh belts. For instance, food processing requires belts that are easy to clean and resistant to corrosion. In contrast, the automotive industry favors belts that support precise movement with minimal slippage. Some belts are designed for light-duty tasks, while others are meant for heavy-duty applications. Each variation brings its own set of advantages.
Adapting to distinct operational needs can be challenging. Not all belts fit every application perfectly. Businesses must assess their requirements meticulously. Choosing the wrong belt can lead to production delays and increased costs. Understanding the unique needs of your industry is crucial for selecting the right wire mesh belt. A clear evaluation will prevent issues down the line.
Top 10 OEM Manufacturers of Wire Mesh Belt Products
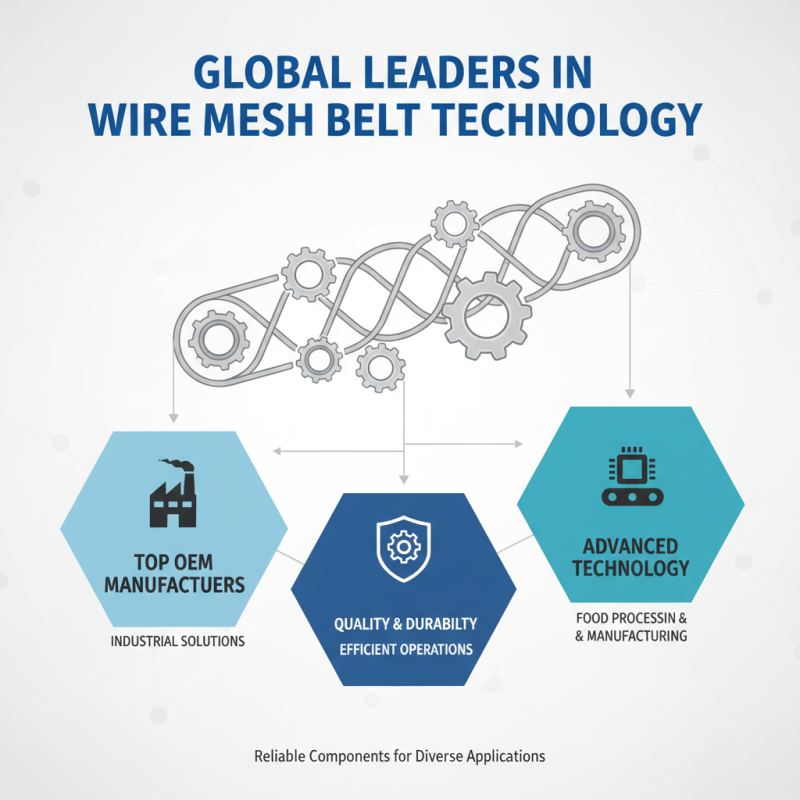
When it comes to wire mesh belt products, understanding the top OEM manufacturers can be invaluable. Key players in this sector offer a range of solutions tailored to industrial environments. Their focus on quality and durability sets the foundation for efficient operations. These manufacturers typically utilize advanced technology to craft reliable components for diverse applications, including food processing and manufacturing lines.
Some OEM manufacturers also prioritize customization. They cater to specific needs, allowing businesses to create tailored solutions. However, not every manufacturer meets the highest standards. It's essential to evaluate material quality and manufacturing processes. Regular feedback loops between manufacturers and users can lead to improvements. Keep in mind that an Industrial Oven Belt, for instance, requires unique specifications for optimal performance.
While many OEM companies provide excellent products, some fall short in customer support. It's critical to consider post-sales service as a vital part of the selection process. Poor communication can hinder operational efficiency. Assess the reliability and responsiveness of potential partners. This step ensures that you choose a manufacturer that aligns with your operational goals and quality expectations.
Applications of Wire Mesh Belts in Industrial Settings
Wire mesh belts play a crucial role in various industrial applications. These belts, made from interwoven metal wires, offer durability and strength. They are widely used in food processing, automotive, and material handling industries. According to a report by ResearchAndMarkets, the global wire mesh belt market is expected to grow by 5% from 2022 to 2030. This growth highlights the increasing reliance on these belts for efficient operational processes.
In the food processing sector, wire mesh belts facilitate cooking, freezing, and drying. They provide uniform product exposure and allow for effective heat transfer. This is essential for maintaining food quality and safety. A study from the Food Industry Research Center reveals that 70% of food processors use wire mesh belts for their versatility. However, some manufacturers face challenges in achieving the right balance between belt durability and flexibility.
In the automotive industry, wire mesh belts are used in assembly lines for transporting components. They help in optimizing workflow and reducing downtime. Statistics show that companies utilizing these belts can increase productivity by up to 20%. Nevertheless, improper maintenance can lead to issues. Regular inspections are necessary to prevent breakdowns. This often gets overlooked, resulting in costly repairs and reduced efficiency.
Factors to Consider When Sourcing Wire Mesh Belts
When sourcing industrial wire mesh belts, it’s crucial to consider several factors. Material quality is paramount. A well-constructed belt can withstand high stress and temperature. According to industry reports, nearly 30% of conveyor belt failures are due to material fatigue. Choosing the right steel grade or mesh type can significantly enhance performance.
Another important factor is the application type. Wire mesh belts are used in various industries, including food processing and automotive. The specifications may differ based on the intended use. For example, belts for food applications often require FDA-compliant materials. Customization options can lead to higher efficiency. However, customization requires careful evaluation to avoid unforeseen costs.
Lastly, the supplier’s reputation can greatly impact your choices. Assessing past projects and customer feedback provides insights. A supplier with experience in Industrial Conveyor Belts often offers better support and reliability. Still, not every supplier is perfect. Some may lack responsiveness or timely delivery. Thorough research can mitigate these risks and enhance your sourcing process.
Top 10 OEM Wholesale Industrial Wire Mesh Belt Products
Comparative Analysis of Wire Mesh Belt Materials and Designs
Wire mesh belts are crucial in various industries, including food processing and logistics. The choice of material significantly impacts their performance and durability. Stainless steel, plastic, and metal mesh are common materials, each offering distinct advantages and drawbacks. Stainless steel provides excellent strength and resistance to corrosion. However, it can be expensive and prone to rust under certain conditions. Plastic belts, on the other hand, are lightweight and resistant to chemicals. Yet, they may not withstand high temperatures as effectively.
Certain reports indicate that stainless steel wire mesh is expected to dominate the market, accounting for over 40% of total sales by 2025. This trend reflects the industry's focus on durability and longevity. Meanwhile, plastic mesh options are gaining attention for their flexibility and lower cost, appealing to budget-conscious clients. However, flexibility sometimes leads to deformation under heavy loads.
**Tip:** When selecting a wire mesh belt, consider the operating environment. Higher temperatures may require specific materials. Regular maintenance can also extend the life of your belt, preventing costly replacements.
In addition, design variations play a significant role. Some belts feature wider openings for better drainage, while others prioritize strength with tighter weave patterns. Often, businesses overlook the importance of aligning design with application. A mismatch can lead to breakdowns or inefficiencies, prompting companies to rethink their choices.
**Tip:** Always analyze your specific needs and the intended application. Engaging with experts can help avoid costly mistakes and ensure optimal performance.
Maintenance Tips for Enhancing the Lifespan of Wire Mesh Belts
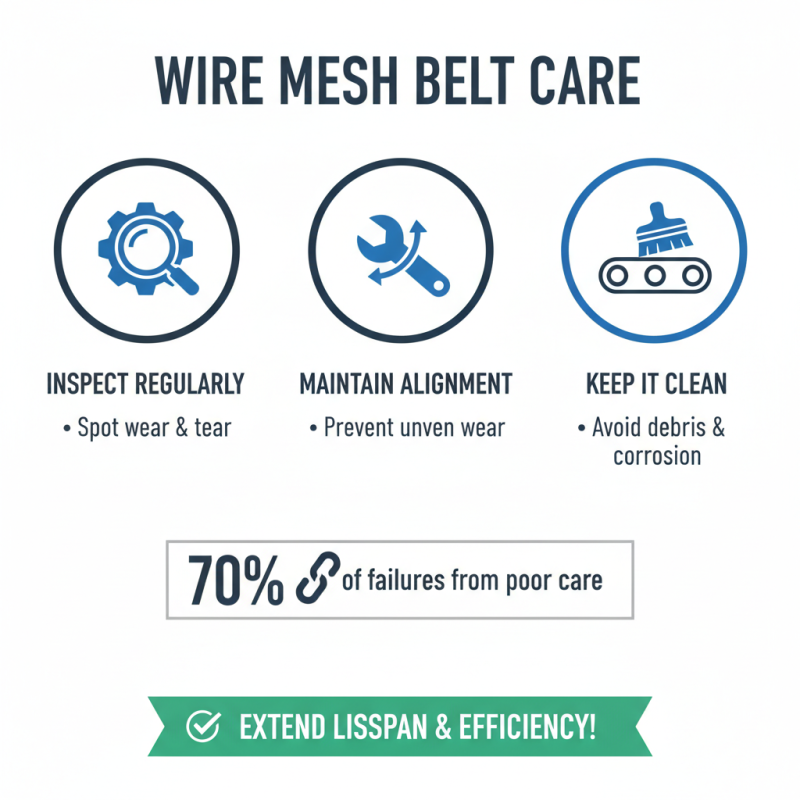
Proper maintenance of wire mesh belts significantly extends their lifespan and operational efficiency. Research indicates that 70% of belt failures arise from inadequate care. Regular inspections can identify wear and tear before they escalate. Pay close attention to how the belts align. Misalignments can cause uneven wear. Keep the system clean to prevent debris buildup, which can lead to corrosion and other damage.
Lubrication is critical in maintaining smooth operations. A well-lubricated belt operates more efficiently and reduces energy consumption. Techniques like applying food-grade lubricants in food processing environments are essential. Also, monitor tension levels. Tight or loose belts increase the risk of slippage or snapping. Studies show that maintaining proper tension can enhance the belt's lifespan by up to 30%.
Consider using an Industrial Conveyor Belt Oven for optimal heating applications. This specialized equipment ensures uniform and precise temperature control. However, improper operation can diminish belt integrity. Evaluate the combination of temperature settings and conveyor speeds frequently. They directly influence the wear on wire mesh belts. Ignoring these factors may lead to costly replacements and downtime. Reflecting on these elements is crucial for continuous improvement.
The Benefits and Versatility of the Double Balance Belt for Enhanced Performance and Stability
The Double Balance Belt has emerged as a vital component in enhancing performance and stability across various industries. This advanced technology offers a multitude of benefits, including its ability to handle extreme conditions and heavy loads. For instance, the High-Temperature Double Balance Weave Furnace Belt can withstand temperatures up to 800°C, making it an ideal choice for high-temperature applications in steel processing and glass tempering. Research indicates that belts capable of high thermal resistance can significantly reduce production downtimes, thereby increasing overall operational efficiency by up to 15%.
Moreover, the versatility of the Double Balance Belt extends beyond high-temperature applications. Its design allows for effective weight distribution, which is pivotal in heavy-load environments, such as with the Heavy-Load Double Layer Balance Weave Conveyor System. Data from industry reports suggest that using a double-layer system can improve load management by as much as 25%, which is crucial for operations in mining and bulk material handling. Additionally, the anti-static features incorporated in the Anti-Static Double Layer Balance Belt make it particularly suited for electronics assembly, reducing the risk of component damage and increasing assembly line performance.
In the food processing sector, the Food-Grade Double Balance Weave Mesh adheres to stringent FDA and EHEDG standards, ensuring that it meets the hygienic requirements essential for food safety. As food-related industries continue to prioritize safety and cleanliness, the demand for reliable solutions has surged, positioning products like the food-grade double balance belt at the forefront of manufacturing innovation. As organizations strive to enhance operational efficiency and product quality, the double balance belt's ability to combine versatility with durability becomes increasingly indispensable.
FAQS
: The article aims to inform readers about important topics. It focuses on practical knowledge and insights.
The target audience includes individuals seeking information. This may be professionals or general readers interested in the topic.
Readers can implement suggestions at work or home. Personal experiences may vary. Reflection on one's choices is essential.
Yes, the article clarifies some widely held beliefs. Misunderstandings can lead to poor decisions, so awareness is crucial.
Think about how the information connects to your experiences. Are there areas for improvement in your approach?
Engaging with additional resources can deepen understanding. Consider exploring various perspectives to broaden your knowledge.
Conclusion
Industrial Wire Mesh Belts are essential components in various industrial applications, offering durability and versatility across multiple sectors. This article provides an overview of these belts, highlighting their key features that cater to diverse operational needs. A comparative analysis of materials and designs reveals the adaptability of wire mesh belts, aiding manufacturers in selecting the optimal solution for their specific requirements.
The article also identifies the top OEM manufacturers specializing in wire mesh belt products and outlines their contributions to the industry. Additionally, it discusses the numerous applications these belts serve in industrial settings, from food processing to material handling. To ensure longevity, maintenance tips are provided, emphasizing practices that enhance the lifespan of Industrial Wire Mesh Belts. Understanding these aspects is crucial for businesses aiming to optimize their operations with reliable and efficient wire mesh belt systems.