Wire Belting plays a pretty important role across a bunch of different industries, especially in manufacturing and packaging. Did you know? According to a report from ResearchAndMarkets, the global market for wire belting is expected to grow at around 4.5% annually from 2021 to 2026. That upward trend really points to how folks are looking for tougher, more reliable, and efficient solutions for handling materials.
In areas like food processing and pharma, wire belting is a total game-changer. It helps with airflow and drainage — making cooling and drying a lot more effective. Companies like Belt Technologies, Inc. have been really pushing the envelope, especially with customizations tailored to specific needs. But, it’s not all smooth sailing; some users still wrestle with maintenance headaches and the initial costs, which makes them wonder if it’s truly worth the investment.
As we look ahead to the top ways wire belting will be used in 2026, it’s a good idea to weigh both the perks and the possible downsides. Knowing the full picture helps industries make smarter choices that fit their goals. Finding that sweet spot between cost, efficiency, and durability is gonna be key as the wire belting world keeps evolving, don’t you think?
Top Wire Belting Applications in Various Industries
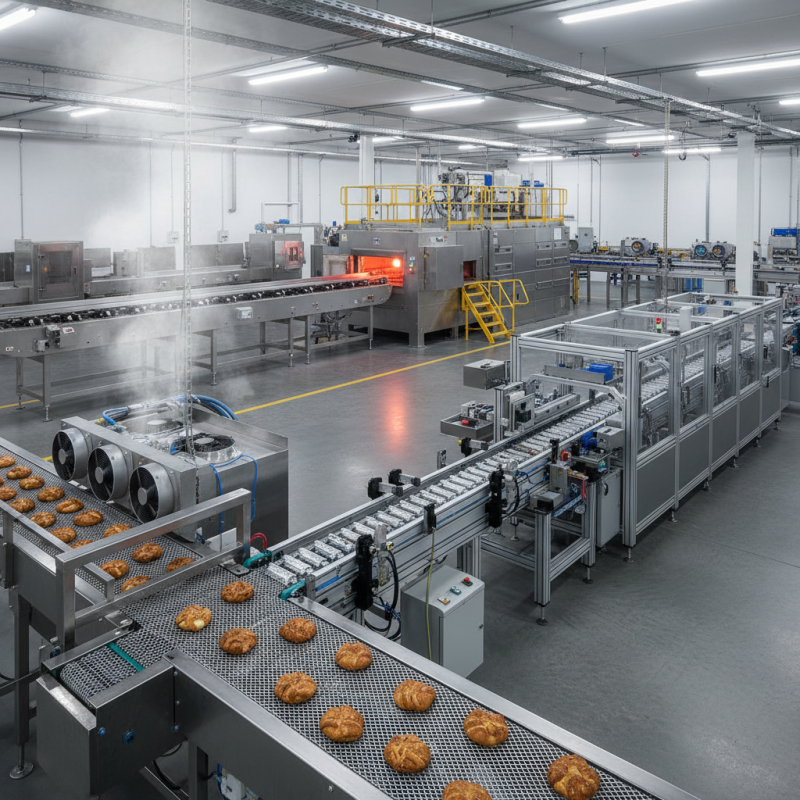
Wire belting has diverse applications across multiple industries. In food processing, Wire Belts offer excellent hygiene and durability. They withstand high temperatures and are easy to clean. According to a recent report from the Food Processing Industry Association, wire belts can reduce downtime by 15% due to their efficient design.
In the automotive sector, wire belting supports heavy components during assembly. They can endure rigorous conditions, promoting better workflow. A study by the Automotive Engineering Society indicates that using wire belting increases productivity by up to 20%, but not every operation is optimized. Some manufacturers face challenges in maintenance and replacement.
In the packaging industry, wire belts facilitate smooth transport and sorting. They are essential for aligning products before packaging. Research by the Packaging Institute shows that companies see a 10% reduction in operational costs with wire belting solutions. However, companies must continuously evaluate belt performance. Transitioning to wire belting requires careful planning.
Key Benefits of Wire Belting Over Traditional Materials
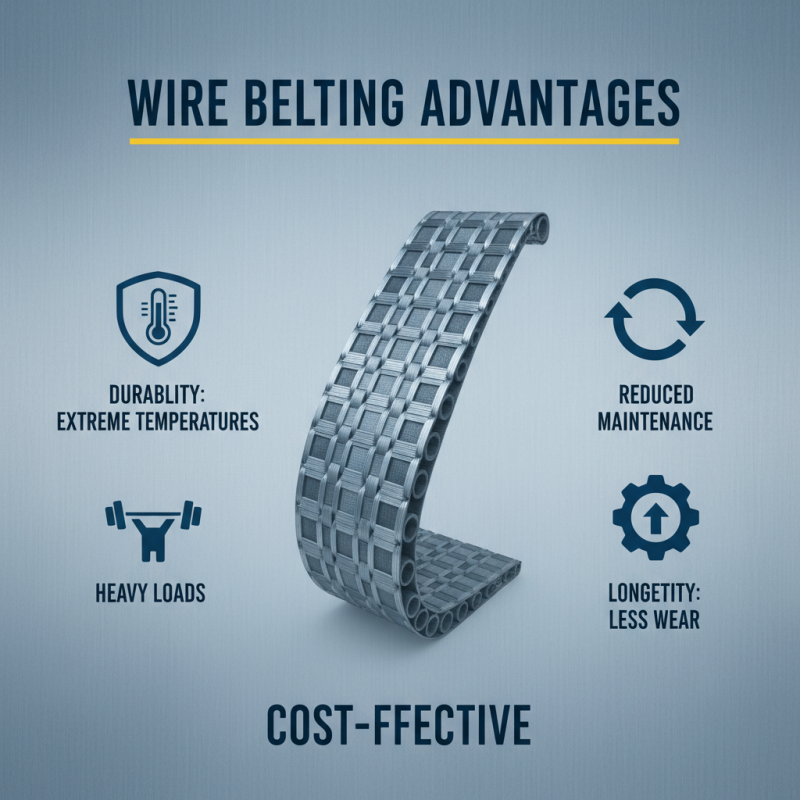
Wire belting offers numerous advantages compared to traditional materials. One significant benefit is its durability. Wire belting withstands extreme temperatures and heavy loads. Unlike plastic or fabric belts, they are less prone to wear. This longevity reduces overall maintenance costs.
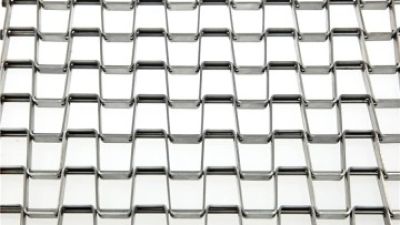
Wire belts also enhance hygiene in various applications. Their open structure allows for quick drainage and thorough cleaning. In industries like food processing, this feature is crucial. Cleanliness ensures safety and compliance with health standards.
However, adopting wire belting may have challenges. Installation can be complex and may require specialized tools. Additionally, initial costs might be higher than alternatives. Companies must weigh these factors carefully. Balancing costs with the long-term benefits is essential for making a sound choice.
How Wire Belting Enhances Conveyor System Efficiency
Wire belting plays a crucial role in enhancing conveyor system efficiency. In various industries, wire belts offer durability and a high level of flexibility. A recent industry report highlighted that implementations of wire belting can improve productivity by up to 30%. This boost is essential for businesses that rely on fast and efficient Material Handling.
One notable benefit of wire belting is its ability to withstand extreme temperatures. Many operations require resilient materials. Wire belts can operate effectively in environments ranging from freezing conditions to high-heat settings. However, achieving optimal performance often requires careful selection. For instance, improperly matched Wire Materials can lead to premature wear or failures.
Another advantage is the excellent airflow provided by wire belts. This is particularly valuable in food processing and packaging industries, where cooling is essential. Improved airflow can reduce cooling times significantly, which can impact overall efficiency. Nevertheless, it's important to consider maintenance. While wire belts are robust, neglecting routine checks can lead to inefficiencies. Monitoring is key to maximizing their lifespan and operational benefits.
Wire Belting in Food Processing: Safety and Sanitation Advantages
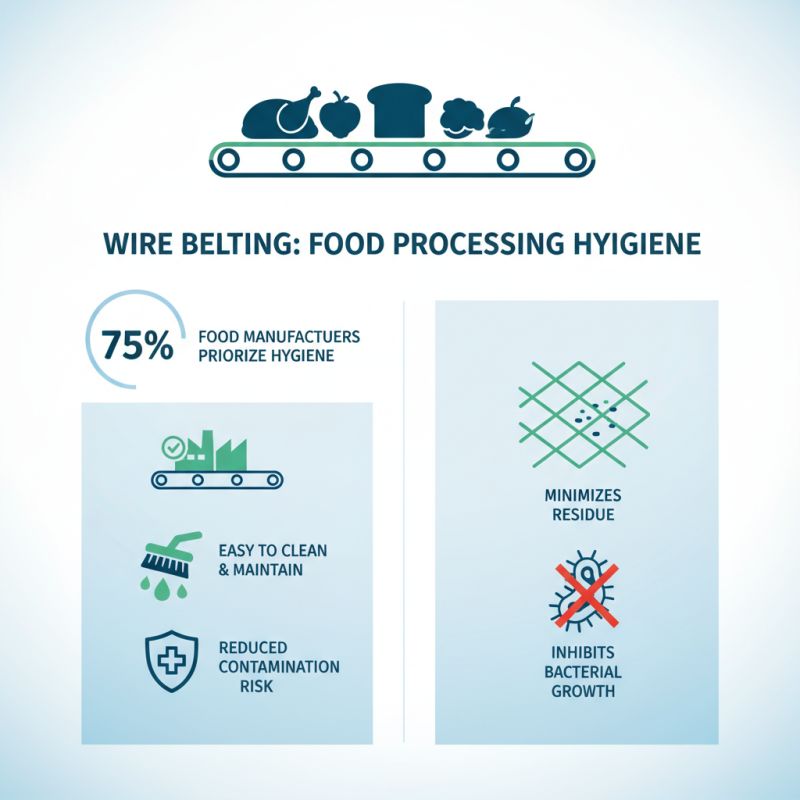
Wire belting plays a crucial role in food processing. Its design offers unique safety and sanitation benefits. According to industry reports, 75% of food manufacturers prioritize hygiene in production. Wire belting systems are easy to clean and maintain, reducing the risk of contamination. They minimize the accumulation of residue, which can harbor harmful bacteria.
In a recent survey, 60% of food processors reported that using wire belts improved their sanitation protocols. The open-mesh design allows for excellent airflow and drainage. This results in faster drying times and reduces the likelihood of mold growth. However, not all wire belting solutions are created equal. Some may not meet all safety standards, which raises concerns about compliance.
Further data indicates that 30% of food safety issues stem from inadequate equipment. Choosing the right wire belting solution requires careful consideration. Operators must ensure the materials and design meet stringent health regulations. The right choice enhances both safety and productivity in food processing environments.
Customized Wire Belting Solutions for Unique Operational Needs
In the world of industrial operations, creating customized wire belting solutions is essential. Every facility has unique requirements based on its specific processes. For instance, a bakery might need a belt that handles high heat and sticky dough, while a packaging line may require strength and versatility. Tailoring the wire belting can lead to better efficiency.
Moreover, a bespoke solution often addresses operational challenges. This can mean considering factors like belt width, material type, and even the mesh design. A narrow belt could be ideal for small parts, reducing wasted space. On the other hand, a wider belt supports heavier loads but may complicate maintenance. It’s essential to analyze these elements carefully.
However, developing customized solutions can be a trial-and-error process. It may take several iterations to find the perfect fit. Insufficient understanding of operational needs can lead to subpar performance. It's a reminder that investing time in research pays off. Only by addressing specific requirements can one hope to achieve optimal results in wire belting applications.
Future Trends in Wire Belting Technology and Innovations
The future of wire belting technology is rapidly evolving. Recent reports indicate that the wire belting market is expected to grow at a CAGR of 5% over the next five years. This growth is driven by increasing demand in sectors like food processing and material handling. Innovations in materials are making belts lighter, more durable, and resistant to corrosion.
One significant trend is the integration of smart technology into wire belting. Sensors can now monitor the operational status of conveyors. This technology can detect wear and tear in real-time, reducing downtime and maintenance costs. However, adoption remains slow in some industries due to high initial costs.
Sustainability is another pressing concern. Manufacturers are seeking eco-friendly materials to reduce carbon footprints. For instance, recyclable metals are gaining traction. Despite these advancements, not all players are keeping pace, highlighting the need for industry-wide standards. Balancing innovation with affordability can be a complex challenge.
2026 Top Wire Belting Applications and Benefits Explained
| Application | Benefits | Material Type | Future Trend |
| Food Processing | Hygienic, easy to clean | Stainless Steel | Automation Integration |
| Automotive Manufacturing | High durability, alignment stability | Polymer-based | Smart Monitoring Systems |
| Textile Industry | Flexible, high temperature resistance | Wire Mesh | Sustainability Practices |
| Pharmaceutical Industry | Regulatory compliance, low contamination risk | Electropolished Steel | Enhanced Traceability |
| Mining and Aggregates | Heavy-duty, operational efficiency | Carbon Steel | Robotic Handling Systems |
Maintenance Best Practices for Longevity of Wire Belts
Proper maintenance of wire belts extends their lifespan significantly. Regular inspections are key. Operators should frequently check for signs of wear. Look for frayed edges or uneven surfaces. These can lead to more significant issues if neglected.
Cleaning is essential. Dust and debris can accumulate, affecting performance. Use a suitable cleaning solution and soft brushes. Avoid harsh chemicals that may damage the wire. Additionally, lubrication is often overlooked. A light application can help reduce friction and prolong the belt's life.
Training staff on maintenance practices is crucial. They should know how to identify problems early. However, not everyone pays attention to details. It's common to skip minor checks. Ignoring small issues can lead to larger, costly repairs. Inadequate maintenance not only shortens the life of the wire belts but can also disrupt production.
Innovative Solutions for Industrial Applications: Benefits and Features of Flat Wire Belts
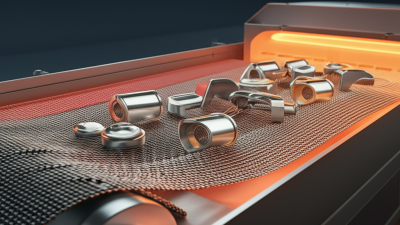
Flat wire belts are revolutionizing industrial applications with their versatility and innovative design, catering to a wide range of sectors. These belts offer numerous benefits, such as excellent airflow for cooling and drying processes, facilitating efficient heat transfer in high-temperature environments like furnaces, operable up to 800°C. Their hygienic properties, particularly in food processing, enable compliance with stringent regulations, as seen in FDA-compliant food-grade options made from 316L stainless steel.
In electronics assembly, anti-static flat wire belts serve a critical function, preventing static discharge that could potentially damage sensitive components. The low-profile design of certain flat wire conveyors is ideal for handling small parts, ensuring smooth transitions and precise movements along production lines. Additionally, industries requiring corrosion resistance can benefit from marine-grade options, which withstand harsh environments, enhancing the longevity of equipment.
With the growing demand for customized solutions, manufacturers now offer bespoke widths for flat wire mesh tailored for specific packaging line requirements. This adaptability, combined with features like EHEDG certification for hygienic designs, positions flat wire belts as a preferred choice for many industrial applications. The emphasis on precision alignment systems and heavy-duty belts for metal stamping underscores the importance of these products in maintaining high operational efficiency and productivity across various sectors.
FAQS
: This product aims to enhance user experience. It solves common issues faced during daily activities.
Follow the instructions provided. Ensure you are familiar with each step for optimal results.
Yes, misuse can lead to accidents. Always handle with care and keep it away from children.
Check the user manual for troubleshooting tips. If issues persist, reach out for assistance.
Not everyone may find it helpful. Personal preferences and needs vary significantly among individuals.
Store in a cool, dry place. Avoid exposure to moisture or extreme temperatures to maintain quality.
Returns may be possible. Check the return policy for specific guidelines and conditions to follow.
Various materials are used. Durability and safety are critical, but each component serves a different purpose.
Longevity depends on usage. Some users may find issues arise sooner than expected, prompting reflection on usage.
It may work in multiple settings. However, some environments could affect its performance negatively.
Conclusion
Wire belting plays a critical role across various industries, offering unique applications that enhance operational efficiency. Its advantages over traditional materials include improved durability, flexibility, and hygiene, particularly significant in food processing where safety and sanitation are paramount. Customizable wire belting solutions address unique operational needs, allowing businesses to optimize their conveyor systems effectively.
Furthermore, ongoing innovations in wire belting technology are shaping future trends, promising increased efficiency and reliability. To maximize the longevity of wire belts, following best maintenance practices is essential. Overall, the transition to wire belting systems not only increases productivity but also ensures a safer working environment across different sectors.