Leave Your Message
0%

You know, there's a big push worldwide for better, more efficient transport solutions—that's what really drives industries these days. Metal Conveyor Belts, in particular, are game-changers when it comes to boosting productivity. I read somewhere, like a study from Grand View Research, that the entire global conveyor system market was valued at about $8 billion back in 2020. And get this—it’s expected to grow at roughly 4.2% annually between 2021 and 2028. That kind of growth just goes to show how important it is to go for durable, high-quality materials like metal, which can handle the workload reliably. When you think about industries like food processing, automotive, or packaging, the applications for metal conveyor belts are pretty much endless. Their strength and ability to stand up to heavy loads and hot temperatures make them perfect for those tough environments. But, of course, choosing the right products—especially if you're looking for wholesale discounts—is key to keeping costs down without sacrificing quality. Companies like Ashworth Bros. and Dorner Manufacturing really know their stuff—they've got a ton of options tailored to different business needs. That said, it’s not all smooth sailing. Installing and maintaining these systems can be a bit tricky, and the initial costs can be pretty high. Plus, if you don’t keep up with regular maintenance, performance might dip, which could end up costing you more in the long run. So, yeah—when you’re thinking about metal conveyor belts, it’s definitely worth weighing the pros and cons carefully to make sure you’re making the right move for your business.
Best Wholesale Discount Metal Conveyor Belt Products for Efficient Transport?

Understanding Metal Conveyor Belts and Their Applications

Best Wholesale Discount Metal Conveyor Belt Products for Efficient Transport?

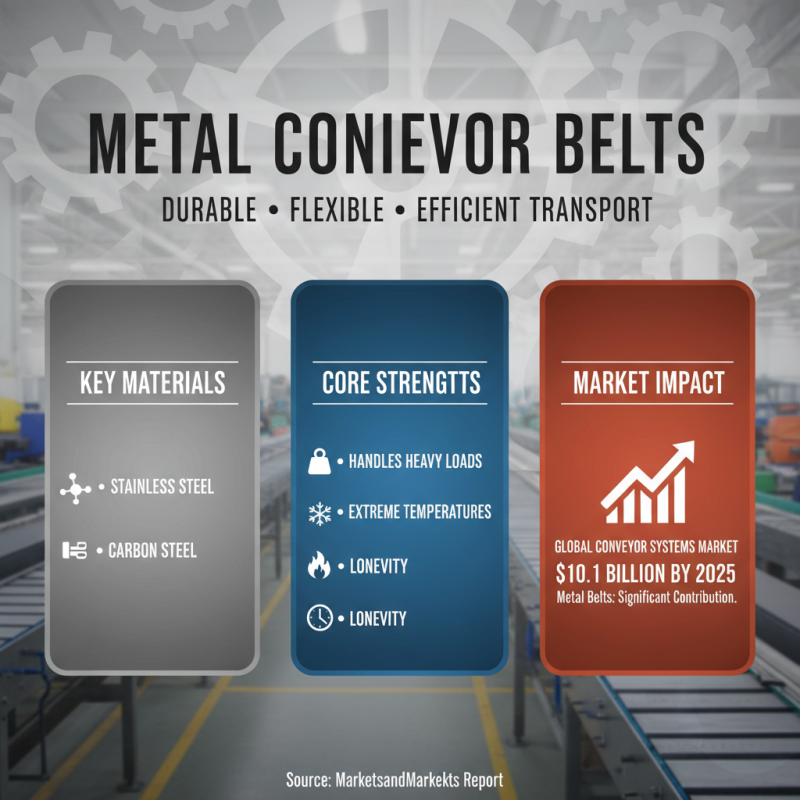
Metal conveyor belts play a crucial role in various industries. They offer durability, flexibility, and efficient transport. These belts are made from materials such as stainless steel and carbon steel. Their strength allows them to handle heavy loads and operate in extreme temperatures. According to a report by MarketsandMarkets, the global conveyor systems market is expected to reach $10.1 billion by 2025, with metal conveyor belts making a significant contribution.

Industries like food processing and automotive rely heavily on these belts. Metal conveyor belts provide hygiene and easy cleaning, essential for food safety. In automotive manufacturing, they ensure precise and efficient transport of parts. Surprisingly, many companies overlook the importance of proper maintenance for these systems. Regular inspection can prevent costly downtime and improve longevity.

Applications extend beyond manufacturing. Metal conveyor belts are found in packaging and distribution centers too. The versatility of design allows them to be customized for different transport needs. Some industries still use outdated models, limiting their efficiency. Embracing innovation can lead to improved operational performance and reduced costs.

Benefits of Using Wholesale Discount Metal Conveyor Belt Products

Wholesale discount metal conveyor belt products bring numerous advantages for businesses looking to enhance their transport efficiency. These belts offer durability and strength, making them ideal for heavy loads. Additionally, metal conveyor belts are resistant to extreme temperatures and harsh conditions, ensuring reliable performance in diverse environments.

When selecting conveyor belts, consider the material. Stainless Steel Belts resist corrosion and are easy to clean. This is crucial for food processing or pharmaceutical applications. Always check for customization options. Tailoring the dimensions and features can greatly improve operational efficiency.

Tips: Regular maintenance can extend the life of your conveyor belts. Inspect for any signs of wear or damage routinely. Educating your staff on proper usage also minimizes issues. Lastly, evaluating your conveyor system's layout can uncover hidden inefficiencies. Make adjustments as necessary for a smoother transport process.

Key Factors to Consider When Selecting Metal Conveyor Belts

When selecting metal conveyor belts, several key factors come into play. Consider the environment where the belt will operate. High temperatures or corrosive materials can affect belt longevity. Understanding the nuances of your specific operation is essential. The right choice can mean smooth transport and fewer disruptions.


The material and design of the Metal Conveyor Belt Mesh are crucial. Different applications require different belt types. Choose a mesh that fits your product size and weight. For instance, a finer mesh is ideal for smaller items. Ensure the belt can handle the load without compromising efficiency.


Consult industry experts to gather insights. Their experience can guide you to make informed decisions. Look for data on durability and performance. Real-world feedback can highlight potential issues. Remember, not all metal conveyor belts are created equal. Each application demands careful thought and testing to ensure reliability and effectiveness.

Top Manufacturers of Wholesale Metal Conveyor Belts in the Market

In the bustling world of manufacturing and logistics, efficient transport systems are crucial. Metal conveyor belts play an essential role in streamlining processes. According to industry experts, the global conveyor belt market is projected to reach $7.87 billion by 2026, showing significant growth. The demand for durable and efficient metal conveyor belts is rising, and several manufacturers are leading the way.

Top manufacturers focus on creating belts that withstand heavy loads and harsh environments. Their products are designed with materials that ensure longevity and reliability. Quality assurance is paramount, as it prevents unexpected downtimes. Regular maintenance of these systems can minimize wear and tear, yet many companies overlook this aspect, leading to costly repairs.

Tips: Regularly inspect conveyor systems to catch signs of wear early. Consider materials that provide resistance to corrosion and extreme temperatures. The right metal conveyor belt can significantly improve transport efficiency and reduce costs over time.

Comparative Analysis of Various Metal Conveyor Belt Designs

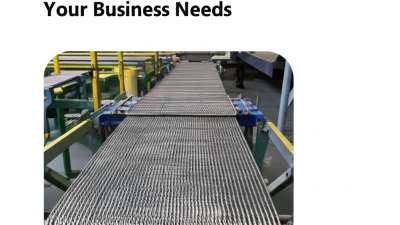
When considering metal conveyor belt designs, a few key features stand out. Metal Mesh Conveyor Belts are known for their durability. These belts can withstand heavy loads and extreme temperatures. Their open structure allows for efficient airflow, which is essential in food processing and drying applications. Different designs may offer varying levels of flexibility, which can impact their effectiveness in tight spaces.

Another crucial factor is the belt’s surface. Smooth surfaces are ideal for transporting small items, while textured surfaces provide better grip for larger loads. However, more grip sometimes leads to wear and tear. It's a balance that manufacturers must carefully consider. Some designs may support faster transport speeds, but they may sacrifice stability in the process.

Evaluating the strengths and weaknesses of each design requires expert knowledge. Accessories, such as sidewalls and cleats, can enhance performance but can also complicate maintenance. Choosing the right design involves understanding the specific needs of your operation. While one style may seem ideal, it is essential to consider the long-term implications of that choice.

Cost Efficiency and Long-Term Value of Metal Conveyor Belts

Best Wholesale Discount Metal Conveyor Belt Products for Efficient Transport?

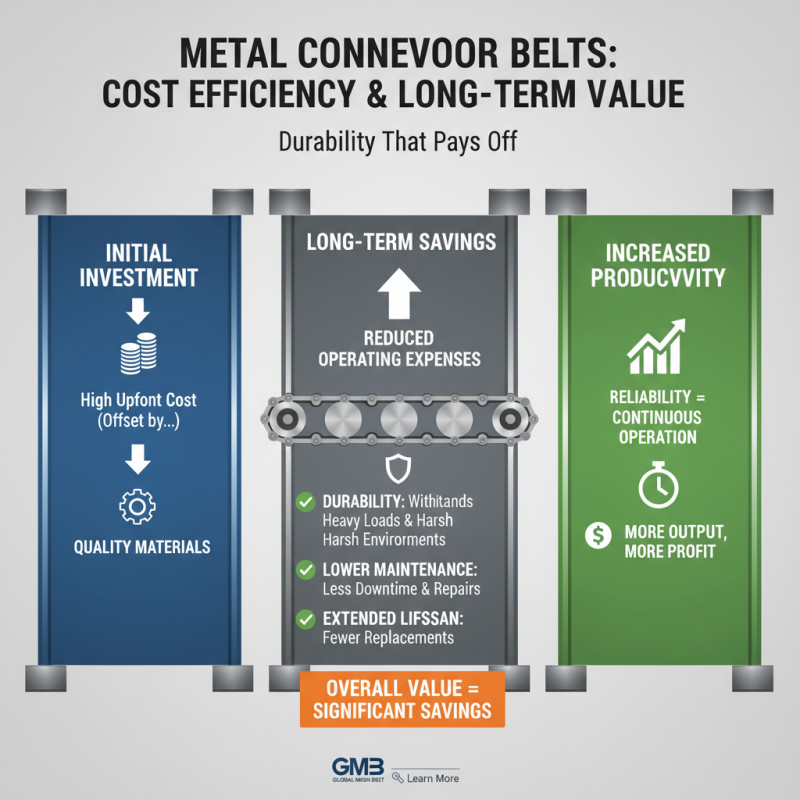
When considering metal conveyor belts, cost efficiency is a major factor. Their durability ensures long-term value. Metal Chain Conveyor Belt systems are designed to withstand heavy loads and harsh environments. This reliability can lead to reduced maintenance costs. Over time, businesses can save significantly on repairs and replacements.

Many companies overlook the initial setup costs associated with metal conveyor systems. While cheaper alternatives may seem attractive, they often lead to frequent breakdowns and inefficiencies. Investing in a Metal Chain Conveyor Belt can streamline operations. Well-constructed belts reduce downtime and improve overall productivity.

Reflecting on the long-term value, it's important to assess wear and tear under real production conditions. Some users find that regular maintenance becomes essential to keep costs manageable. Understanding the balance between upfront investment and future savings is vital. Businesses must weigh these factors carefully to make informed decisions. A comprehensive analysis helps determine if the initial costs justify the benefits in operational efficiency.

Maintenance Tips for Enhancing Conveyor Belt Performance

Maintaining a conveyor belt is essential for ensuring efficient transport in various industries. A well-maintained belt enhances productivity and minimizes downtime. Regular inspection is crucial. Check for wear and tear, especially on edges and joints. Addressing small issues early can prevent larger ones later.

One practical tip is to clean the Metal Annealing Conveyor Belt regularly. Accumulated debris can lead to friction and reduced efficiency. A simple wash can make a big difference. Use a non-abrasive cleaner to avoid damaging the surface. Another detail to consider is the alignment of the belt. Misalignment can cause uneven wear, which may require costly repairs over time.

Lubrication plays a pivotal role too. Ensure proper lubrication at joint points. This reduces friction and extends the belt's lifespan. Over-lubrication can also cause problems, creating unwanted residues. Balancing is key. Employees should be trained to recognize when maintenance is due. Regular training can foster a culture of proactive upkeep and reflection on practices.

Best Wholesale Discount Metal Conveyor Belt Products for Efficient Transport - Maintenance Tips for Enhancing Conveyor Belt Performance

Belt Type Material Load Capacity (lbs) Width (inches) Maintenance Frequency Maintenance Tips
Flat Wire Belt Stainless Steel 1500 24 Weekly Clean regularly to prevent debris build-up.
Modular Plastic Belt Plastic 1200 30 Monthly Inspect for wear and replace damaged modules.
Wire Mesh Belt Galvanized Steel 2500 36 Biweekly Lubricate bearings and check for misalignment.
Chain Driven Belt Carbon Steel 2000 24 Every 6 months Check for chain tension and wear on sprockets.

FAQS

: What are the main benefits of using metal conveyor belts?

: Metal conveyor belts offer durability, strength, and resistance to extreme temperatures. They enhance transport efficiency.

How can stainless steel belts benefit food processing?

Stainless steel belts resist corrosion and are easy to clean. This makes them ideal for food safety.

Why is regular maintenance important for conveyor belts?

Regular maintenance extends the lifespan of belts. It minimizes wear and prevents costly repairs.

What should I consider when selecting a conveyor belt?

Consider the material and customization options. Tailored dimensions can improve efficiency significantly.

How often should conveyor systems be inspected?

Inspect regularly for wear and damage. Routine checks help catch issues early.

Can adjusting the conveyor layout improve efficiency?

Yes, evaluating the conveyor system layout can unveil hidden inefficiencies. Adjusting it can lead to smoother transport.

What happens if maintenance is overlooked?

Overlooking maintenance can lead to unexpected downtimes. This results in increased operational costs.

Are metal conveyor belts suitable for harsh environments?

Yes, they are designed to withstand harsh conditions. This reliability is crucial for efficient transport.

Is customizing conveyor belts necessary?

Customization is not always necessary, but it can greatly enhance operational efficiency.

What materials should I avoid for conveyor belts?

Avoid materials that lack corrosion resistance. These can lead to shorter lifespan and increased costs.

Conclusion

Metal conveyor belts are essential components in various industries, offering efficient transport solutions for a wide range of applications. Understanding their unique features and benefits is crucial when selecting the right product. Wholesale discount metal conveyor belts provide significant cost savings and long-term value, making them an attractive option for businesses looking to enhance their operations.

When choosing a metal conveyor belt, key factors such as design, durability, and maintenance requirements should be considered to ensure optimal performance. Additionally, a comparative analysis of different designs highlights their suitability for specific tasks, underscoring the importance of selecting the right type for one's needs. Proper maintenance further improves the efficiency and longevity of metal conveyor belts, contributing to a smooth and cost-effective transport process in various industrial settings.
Aria

Aria

Aria is a dedicated marketing professional at Jiangsu Huada Metal Mesh Belt Co., Ltd., a pioneering manufacturer of metal conveyor belts in China. With a deep expertise in the industry, Aria is committed to showcasing the precision-engineered wire mesh belts and chain-driven systems that the......
Previous Top Heavy Duty Wire Mesh Belt Solutions for Global Buyers?