
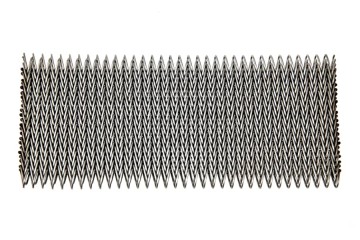
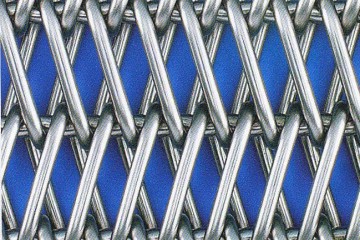
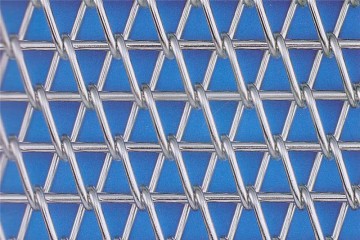
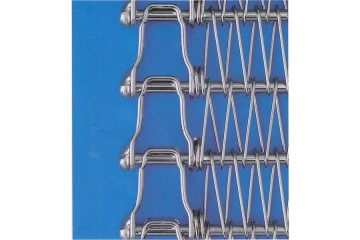


China Factory Suppliers: High-Performance Chain Drive Belt for Heavy Duty Material Handling Solutions
Products Description
Chain Driven Conveyor Mesh Belt | Heavy-Duty & Low Maintenance Design
1,500 kg/m chain-driven belts with 304/316 SS. FDA-compliant & corrosion-resistant for automotive/bottling/frozen food lines in harsh environments.
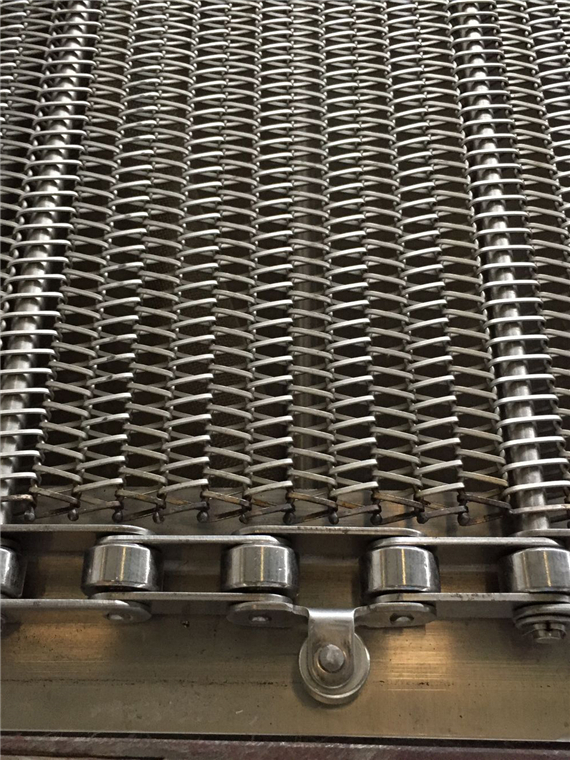
Jiangsu Huada’s chain drive conveyor belts deliver unmatched power transmission efficiency for heavy-load industrial applications. Engineered with forged alloy steel chains and precision-machined rollers, our systems achieve:
- 50% higher load capacity vs. standard belts (up to 500 kg/m²)
- ±0.15mm linear accuracy for precision positioning
- 20% lower energy consumption through optimized link geometry
🏆 Certifications
ISO 9001:2015 | CE Machinery Directive | FDA 21 CFR 177.2600
Technical Advantage
⚙️ Engineered for Heavy Industry
- Tensile strength: 800-1,200 N/mm² (Grade 80/100 chains)
- Surface hardness: HRC 55-60 (Hardened rollers)
🌡️ Extreme Environment Ready
- Temperature range: -40°C to 900°C
- IP69K washdown-rated variants available
🔧 Smart Maintenance Design
- Quick-release tensioners reduce downtime by 40%
- Laser-etched alignment markers for precise tracking
Application Scenarios
| Industry | Application | Huada Solution |
|---|---|---|
| Automotive | Engine block transfer lines | 100kg/m² load capacity chains |
| Mining | Ore sorting conveyors | Tungsten-carbide coated links |
| Food Processing | Meat chilling tunnels | 316L SS with EHEDG compliance |
| Logistics | Parcel sorting systems | High-speed 2m/s variants |
Technical Parameters
| Parameter | Huada Chain Drive Belt | Industry Standard |
|---|---|---|
| Max Load Capacity | 500 kg/m² | 300 kg/m² |
| Pitch Accuracy | ±0.1mm | ±0.3mm |
| Noise Level @3m | ≤68 dB(A) | ≥75 dB(A) |
| Lubrication Interval | 1,000 hours | 500 hours |
Case Study: Automotive Tier-1 Supplier
📈 After implementing Huada’s chain drive systems:
- 30% faster line speeds in chassis assembly
- Zero chain jumps in 18-month operation
- Achieved ISO 50001 energy compliance
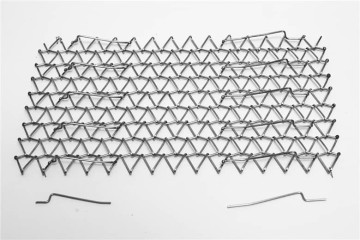
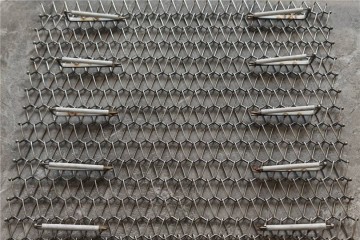
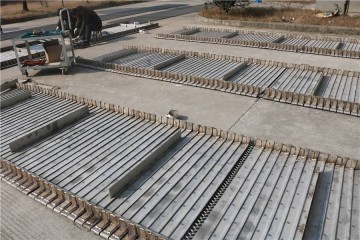
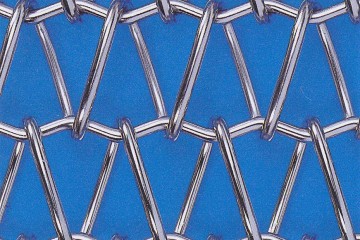
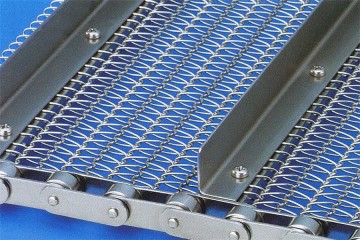
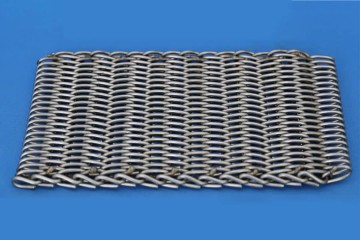
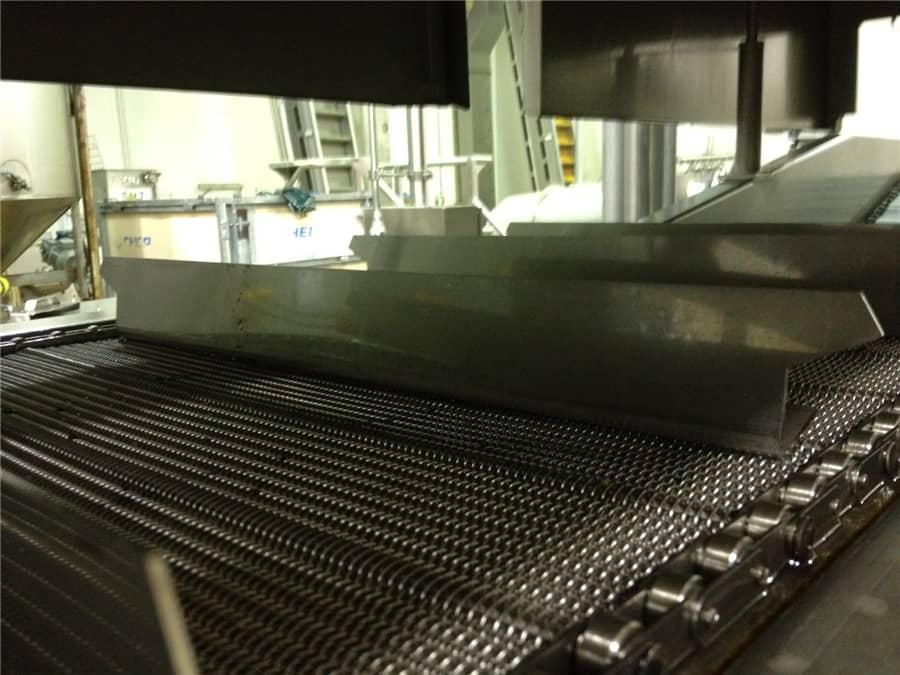
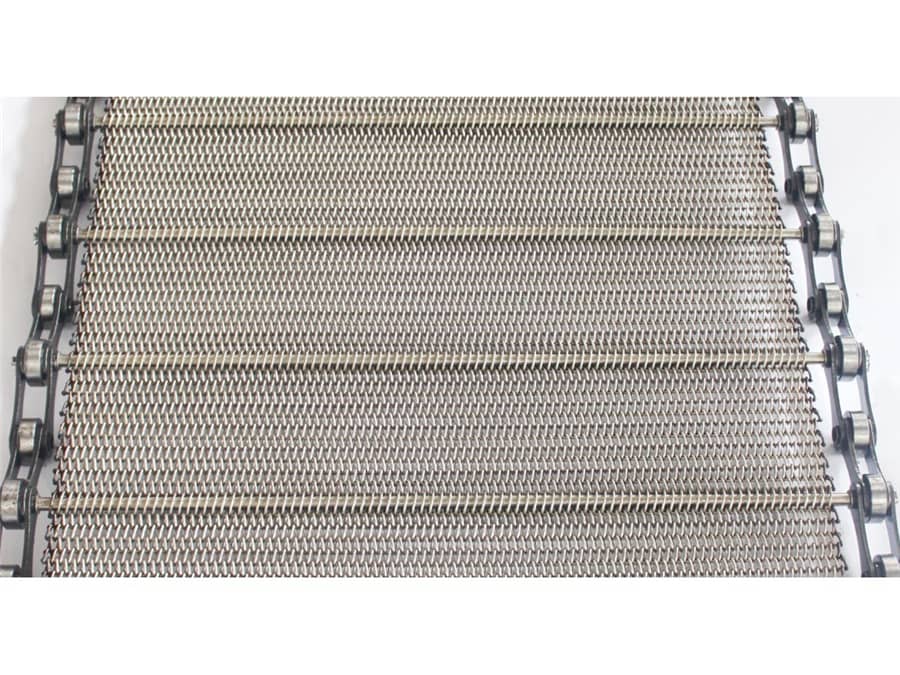
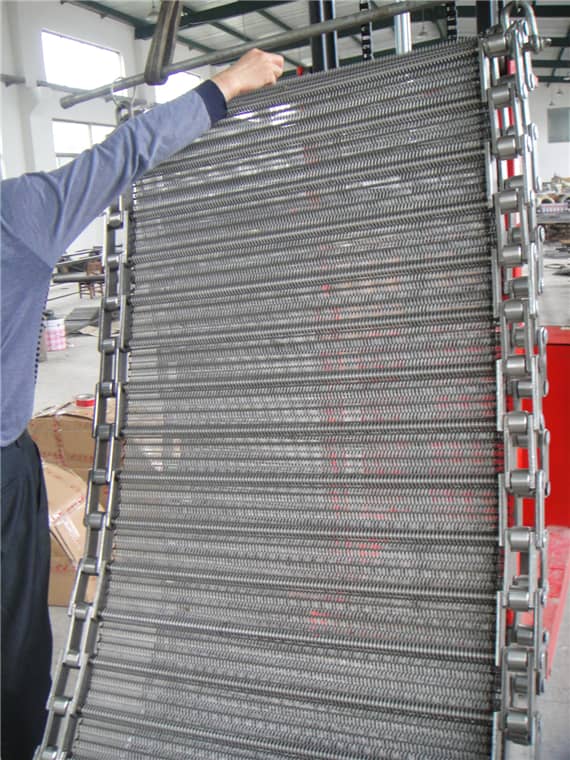
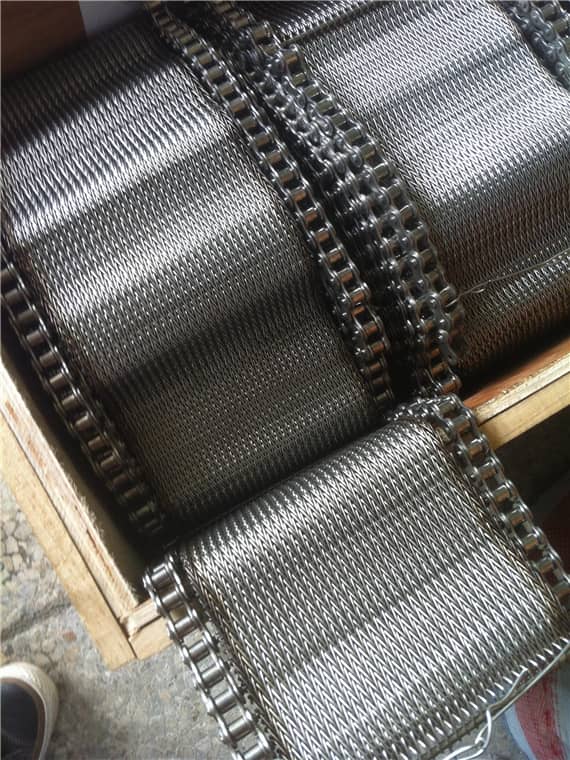
Detail Pictures
Frequently Asked Questions (FAQ)
What is the maximum load capacity of the Huada Chain Drive Belt?
The Huada chain drive belt supports a maximum load capacity of up to 500 kg/m², which is 50% higher than standard industry belts.
What materials are used for these conveyor belts?
They are manufactured using high-quality 304/316 stainless steel with forged alloy steel chains and precision-machined hardened rollers.
Are these conveyor belts suitable for extreme temperatures?
Yes, our extreme environment ready variants can operate efficiently in temperature ranges from -40°C up to 900°C.
Is the belt compliant with food industry standards?
Absolutely. The belts are FDA 21 CFR 177.2600 compliant and we offer 316L SS options with EHEDG compliance, making them perfect for food processing lines.
How does the design help in reducing maintenance time?
The smart maintenance design includes quick-release tensioners that reduce downtime by 40% and laser-etched alignment markers for precise tracking.
What certifications do your chain-driven belts hold?
Our products are certified with ISO 9001:2015, CE Machinery Directive, and FDA standards, ensuring top-tier quality and safety.